-
AboutHebei Linaier Rubber Products Co., Ltd. is located in Duqiao Industrial Zone, Jingxian City, Hebei Province, adjacent to Dezhou, Shandong. Founded in early 2001 with a registered capital of 35 million yuan, it is a scientific

-
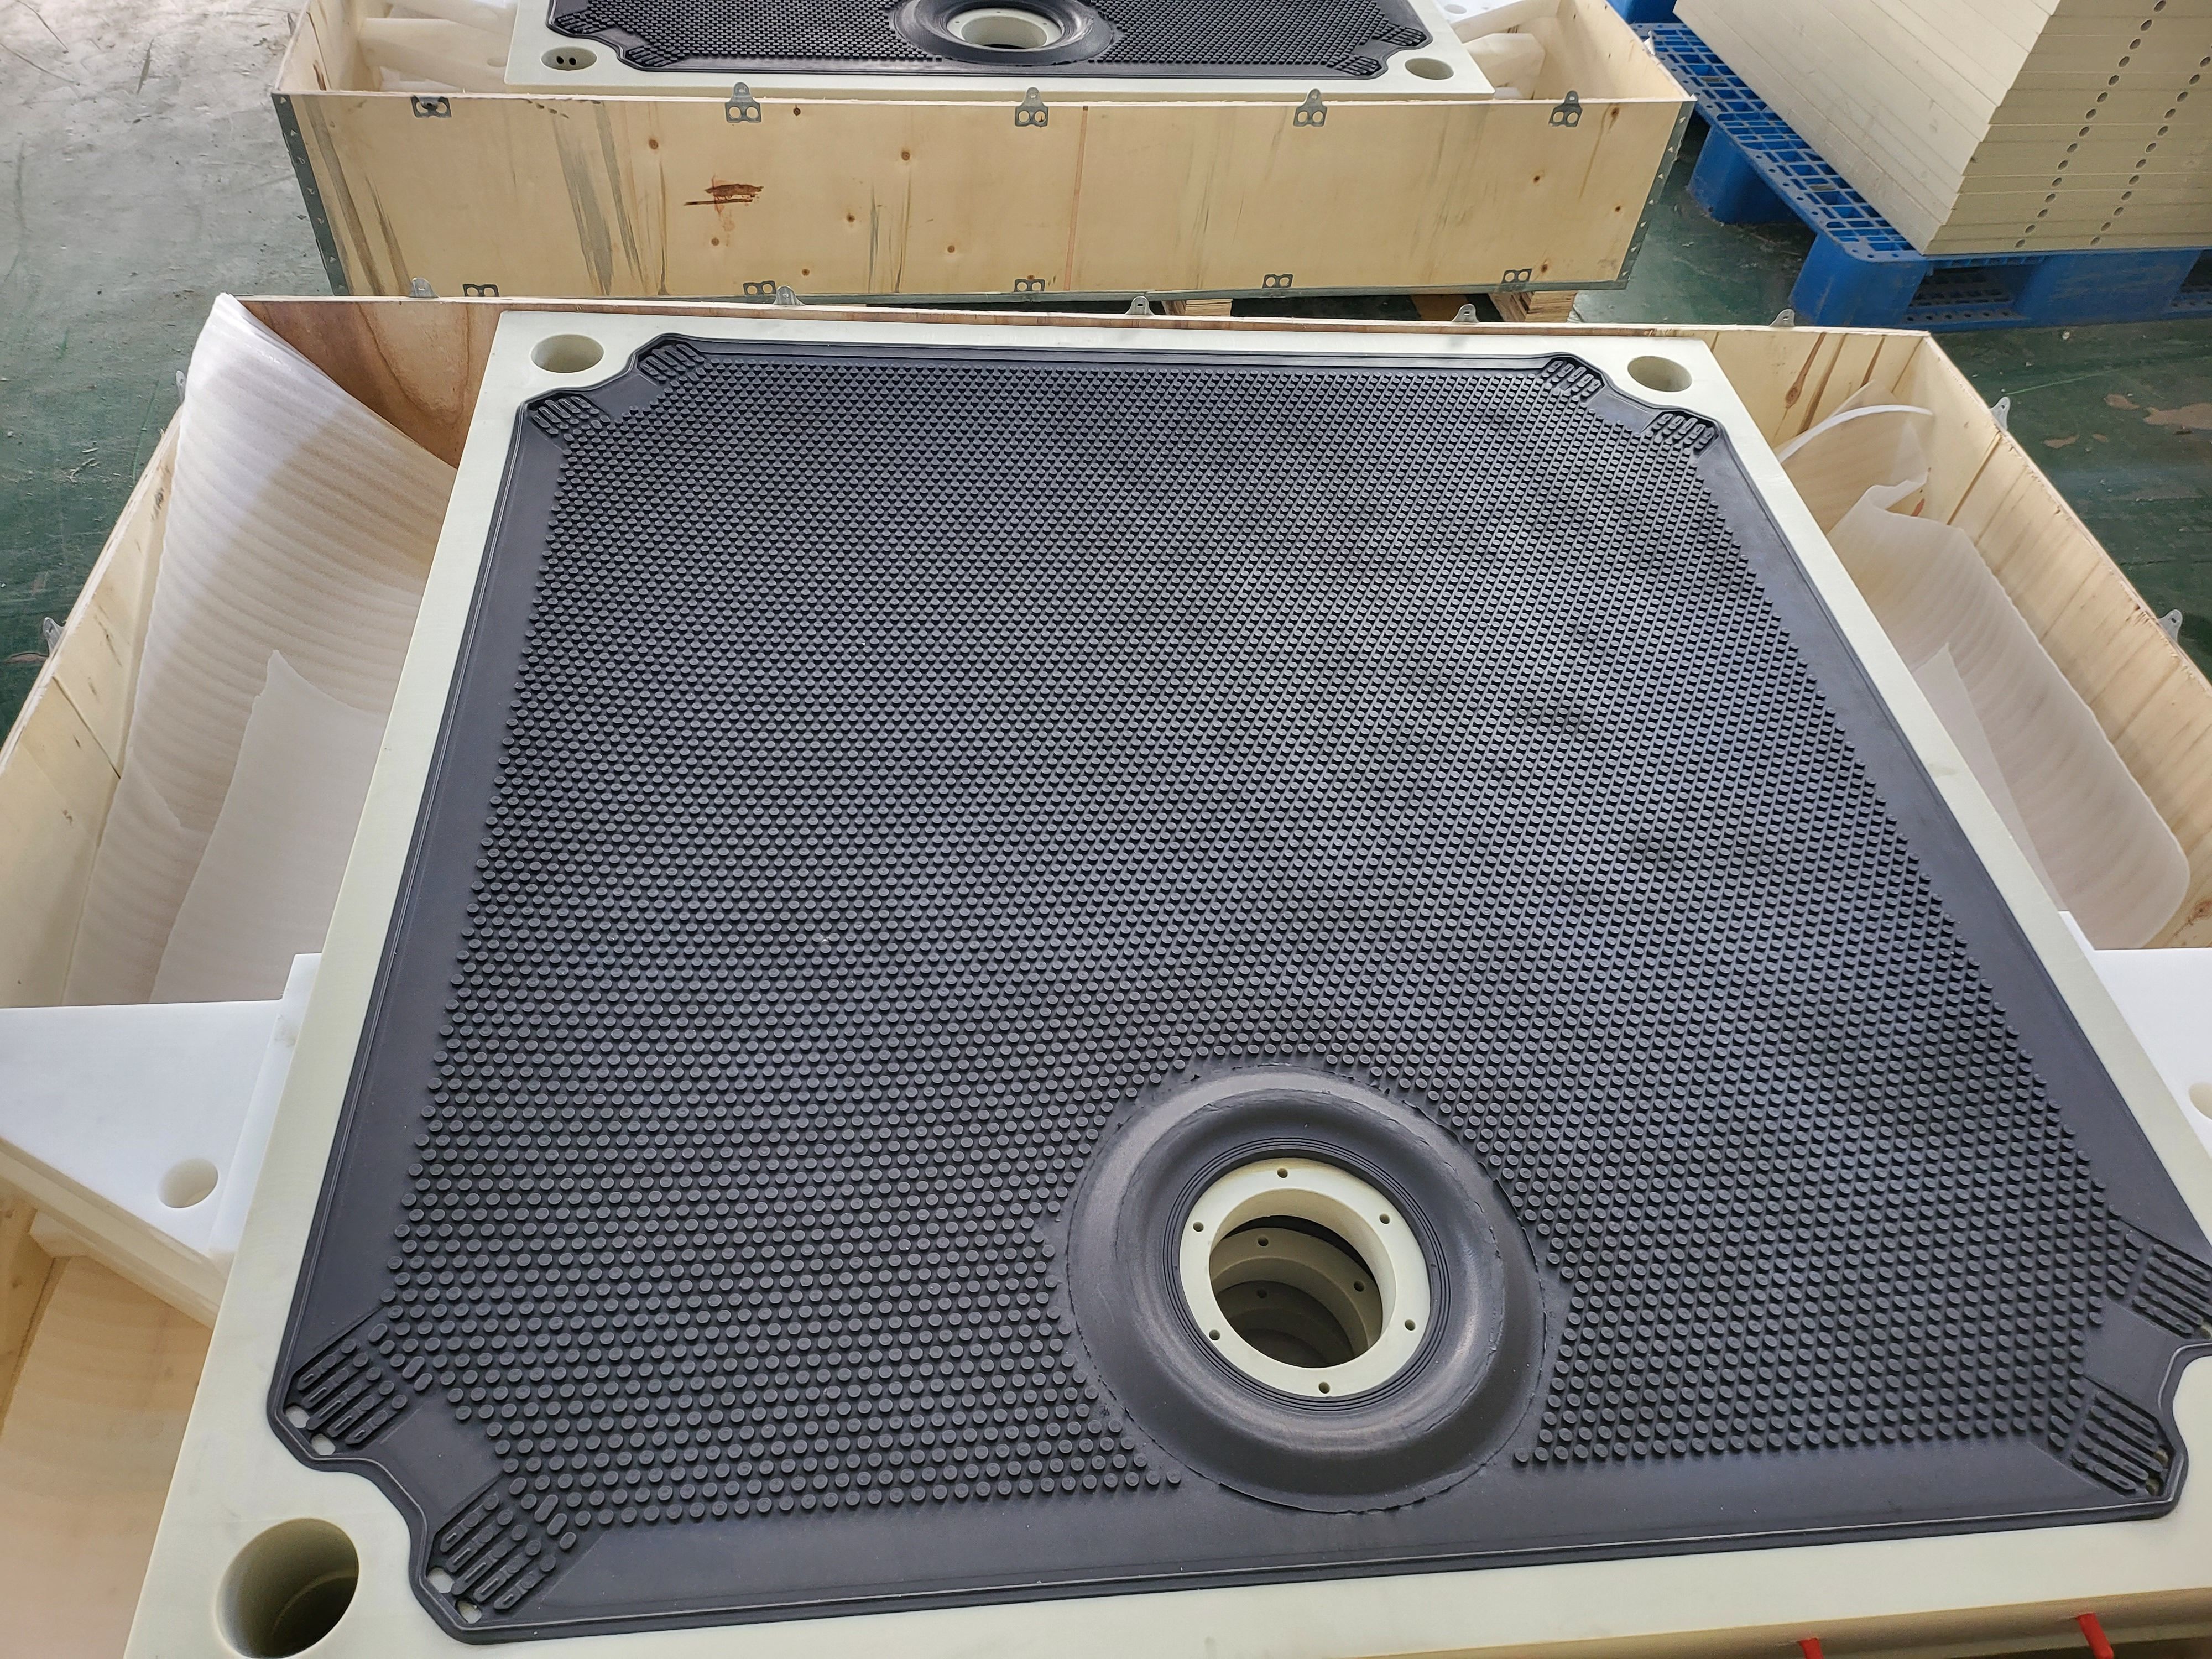
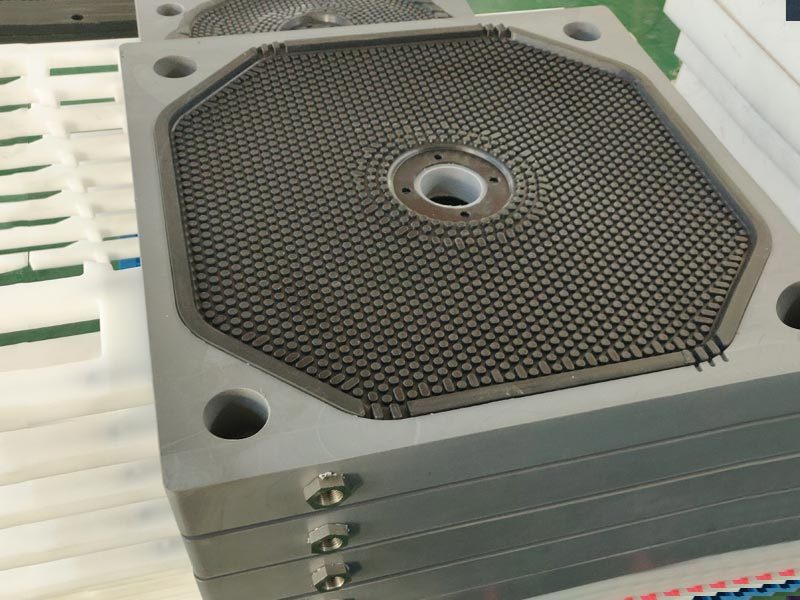
ProductMain products: vertical and horizontal imported and domestic filter plates, diaphragm plates, diaphragms and accessories; pinch valve sleeves and pinch valves and various mining accessories.
-
NewsIn 2013, our company's high-pressure cylinder with phenolic cloth support and guide ring obtained the national key new product certificate, project number: 2013GRA20011; its products in coal cylinders and engineering hydrauli
-
ServiceWe will actively cooperate with more enthusiasm, strengthen internal management, expand the market externally, improve various performance indicators of existing products, and truly achieve our win-win situation!
-
RecruitmentOur company always adheres to the talent concept of "people-oriented", provides a growth platform for talents, and realizes the common growth and development of enterprises and talents.


 Esperanto
 Shqiptare
 Euskara
 Zulu
 Latinus
 Cymraeg
 தமிழ்
 Slovak
 Slovak
 Afrikaans
Release time:
2025-11-11
The Rubber Diaphragm provides flexible sealing, high pressure resistance, and reliable performance for hydraulic, pneumatic, and fluid control systems.
In today’s fast-evolving industrial landscape, where precision, flexibility, and long-term reliability are key to operational excellence, the Rubber Diaphragm stands as a cornerstone of modern sealing and pressure control technology. Designed to perform under extreme conditions, the Rubber Diaphragm ensures consistent performance in hydraulic, pneumatic, and fluid control systems, making it indispensable across a wide range of industries including chemical processing, water treatment, automotive, and energy.
Advanced Design for High-Performance Applications
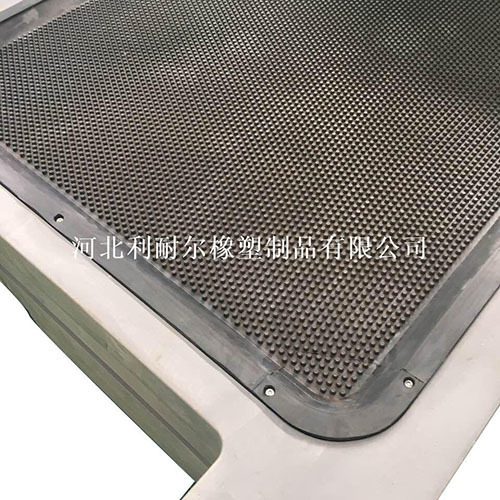
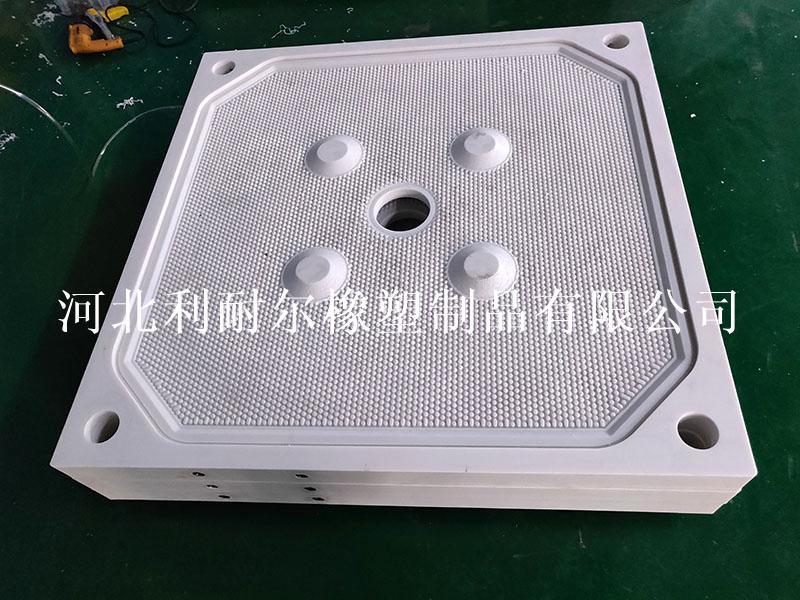
The Rubber Diaphragm is a flexible yet durable sealing component that separates fluids or gases while allowing controlled movement under pressure. Its elasticity and structural integrity make it ideal for applications that require precise pressure regulation and leak-free sealing.
Constructed from premium elastomer materials such as nitrile rubber (NBR), EPDM, fluororubber (FKM), or silicone, the Rubber Diaphragm delivers superior resistance to chemicals, oil, heat, and wear. This versatility ensures reliable performance in high-pressure environments, maintaining stability even under rapid pressure fluctuations or temperature changes.
In diaphragm pumps, control valves, and pneumatic actuators, the Rubber Diaphragm serves as a critical element that directly influences system accuracy and safety. Its exceptional flexibility allows for smooth motion control while preventing leakage or contamination — ensuring high operational efficiency and product consistency.
Precision Engineering Meets Durability
Each Rubber Diaphragm is engineered through advanced molding and vulcanization processes to achieve perfect dimensional stability and uniform thickness. This precision manufacturing guarantees excellent response characteristics and repeatable performance across millions of cycles.
The product’s reinforced fabric layer, often made of nylon or polyester, enhances its strength and resistance to mechanical stress. This innovative structure combines the elasticity of rubber with the tensile strength of fabric, creating a diaphragm that can endure high pressure while maintaining flexibility.
The Rubber Diaphragm also offers excellent sealing properties, minimizing energy loss and ensuring reliable system pressure balance — a critical advantage in demanding applications such as pumps, regulators, and control systems.
Applications Across Multiple Industries
The Rubber Diaphragm finds wide application in industries where precision and durability are essential:
Water and Wastewater Treatment: Ensures reliable flow control in diaphragm valves and dosing systems.
Chemical and Petrochemical Plants: Provides excellent resistance to aggressive media and temperature extremes.
Automotive Systems: Used in braking systems, fuel pumps, and pressure regulators for safe, efficient operation.
Food and Pharmaceutical Processing: Made from food-grade materials to ensure hygiene and compliance with safety standards.
Energy and Power Plants: Maintains stability in control valves and actuators under varying loads and pressures.
This wide applicability demonstrates the Rubber Diaphragm’s adaptability and critical role in ensuring smooth, precise, and safe industrial operations.
Key Advantages and Technical Features
Excellent Sealing Performance: Prevents leakage and contamination in liquid or gas systems.
High Flexibility and Strength: Withstands repeated cycles of pressure and movement without deformation.
Chemical and Temperature Resistance: Operates effectively in aggressive or high-temperature environments.
Customizable Designs: Available in various diameters, thicknesses, and materials to suit specific industry needs.
Long Service Life: Reinforced fabric layers extend durability and reduce maintenance frequency.
These key attributes make the Rubber Diaphragm a preferred solution for industries that prioritize reliability, performance, and cost efficiency.
Sustainability and Innovation
As industries move toward sustainability, the Rubber Diaphragm contributes to eco-friendly production by reducing energy waste, minimizing fluid loss, and ensuring efficient system operation. Its long lifespan decreases material replacement frequency, aligning with global environmental goals.
Furthermore, modern production techniques now allow the use of recyclable and low-emission materials in diaphragm manufacturing, reducing the carbon footprint associated with industrial sealing components.
By integrating innovative materials and precision technology, the Rubber Diaphragm continues to evolve as a crucial component in next-generation fluid and pressure control systems.
A New Benchmark for Industrial Performance
The Rubber Diaphragm represents more than just a sealing element — it embodies the advancement of industrial technology through intelligent design, material innovation, and precision manufacturing. Its balance of strength, flexibility, and chemical resistance positions it as a vital component in modern mechanical and fluid systems.
For engineers, manufacturers, and industrial operators, adopting the Rubber Diaphragm means gaining access to enhanced efficiency, reduced maintenance costs, and reliable operation under the toughest conditions.
As global industries continue to prioritize performance and sustainability, the Rubber Diaphragm will remain an essential innovation driving progress in fluid control and pressure management. It stands as a testament to how material science and engineering excellence can empower modern industry — one seal at a time.
Related News