-
AboutHebei Linaier Rubber Products Co., Ltd. is located in Duqiao Industrial Zone, Jingxian City, Hebei Province, adjacent to Dezhou, Shandong. Founded in early 2001 with a registered capital of 35 million yuan, it is a scientific

-
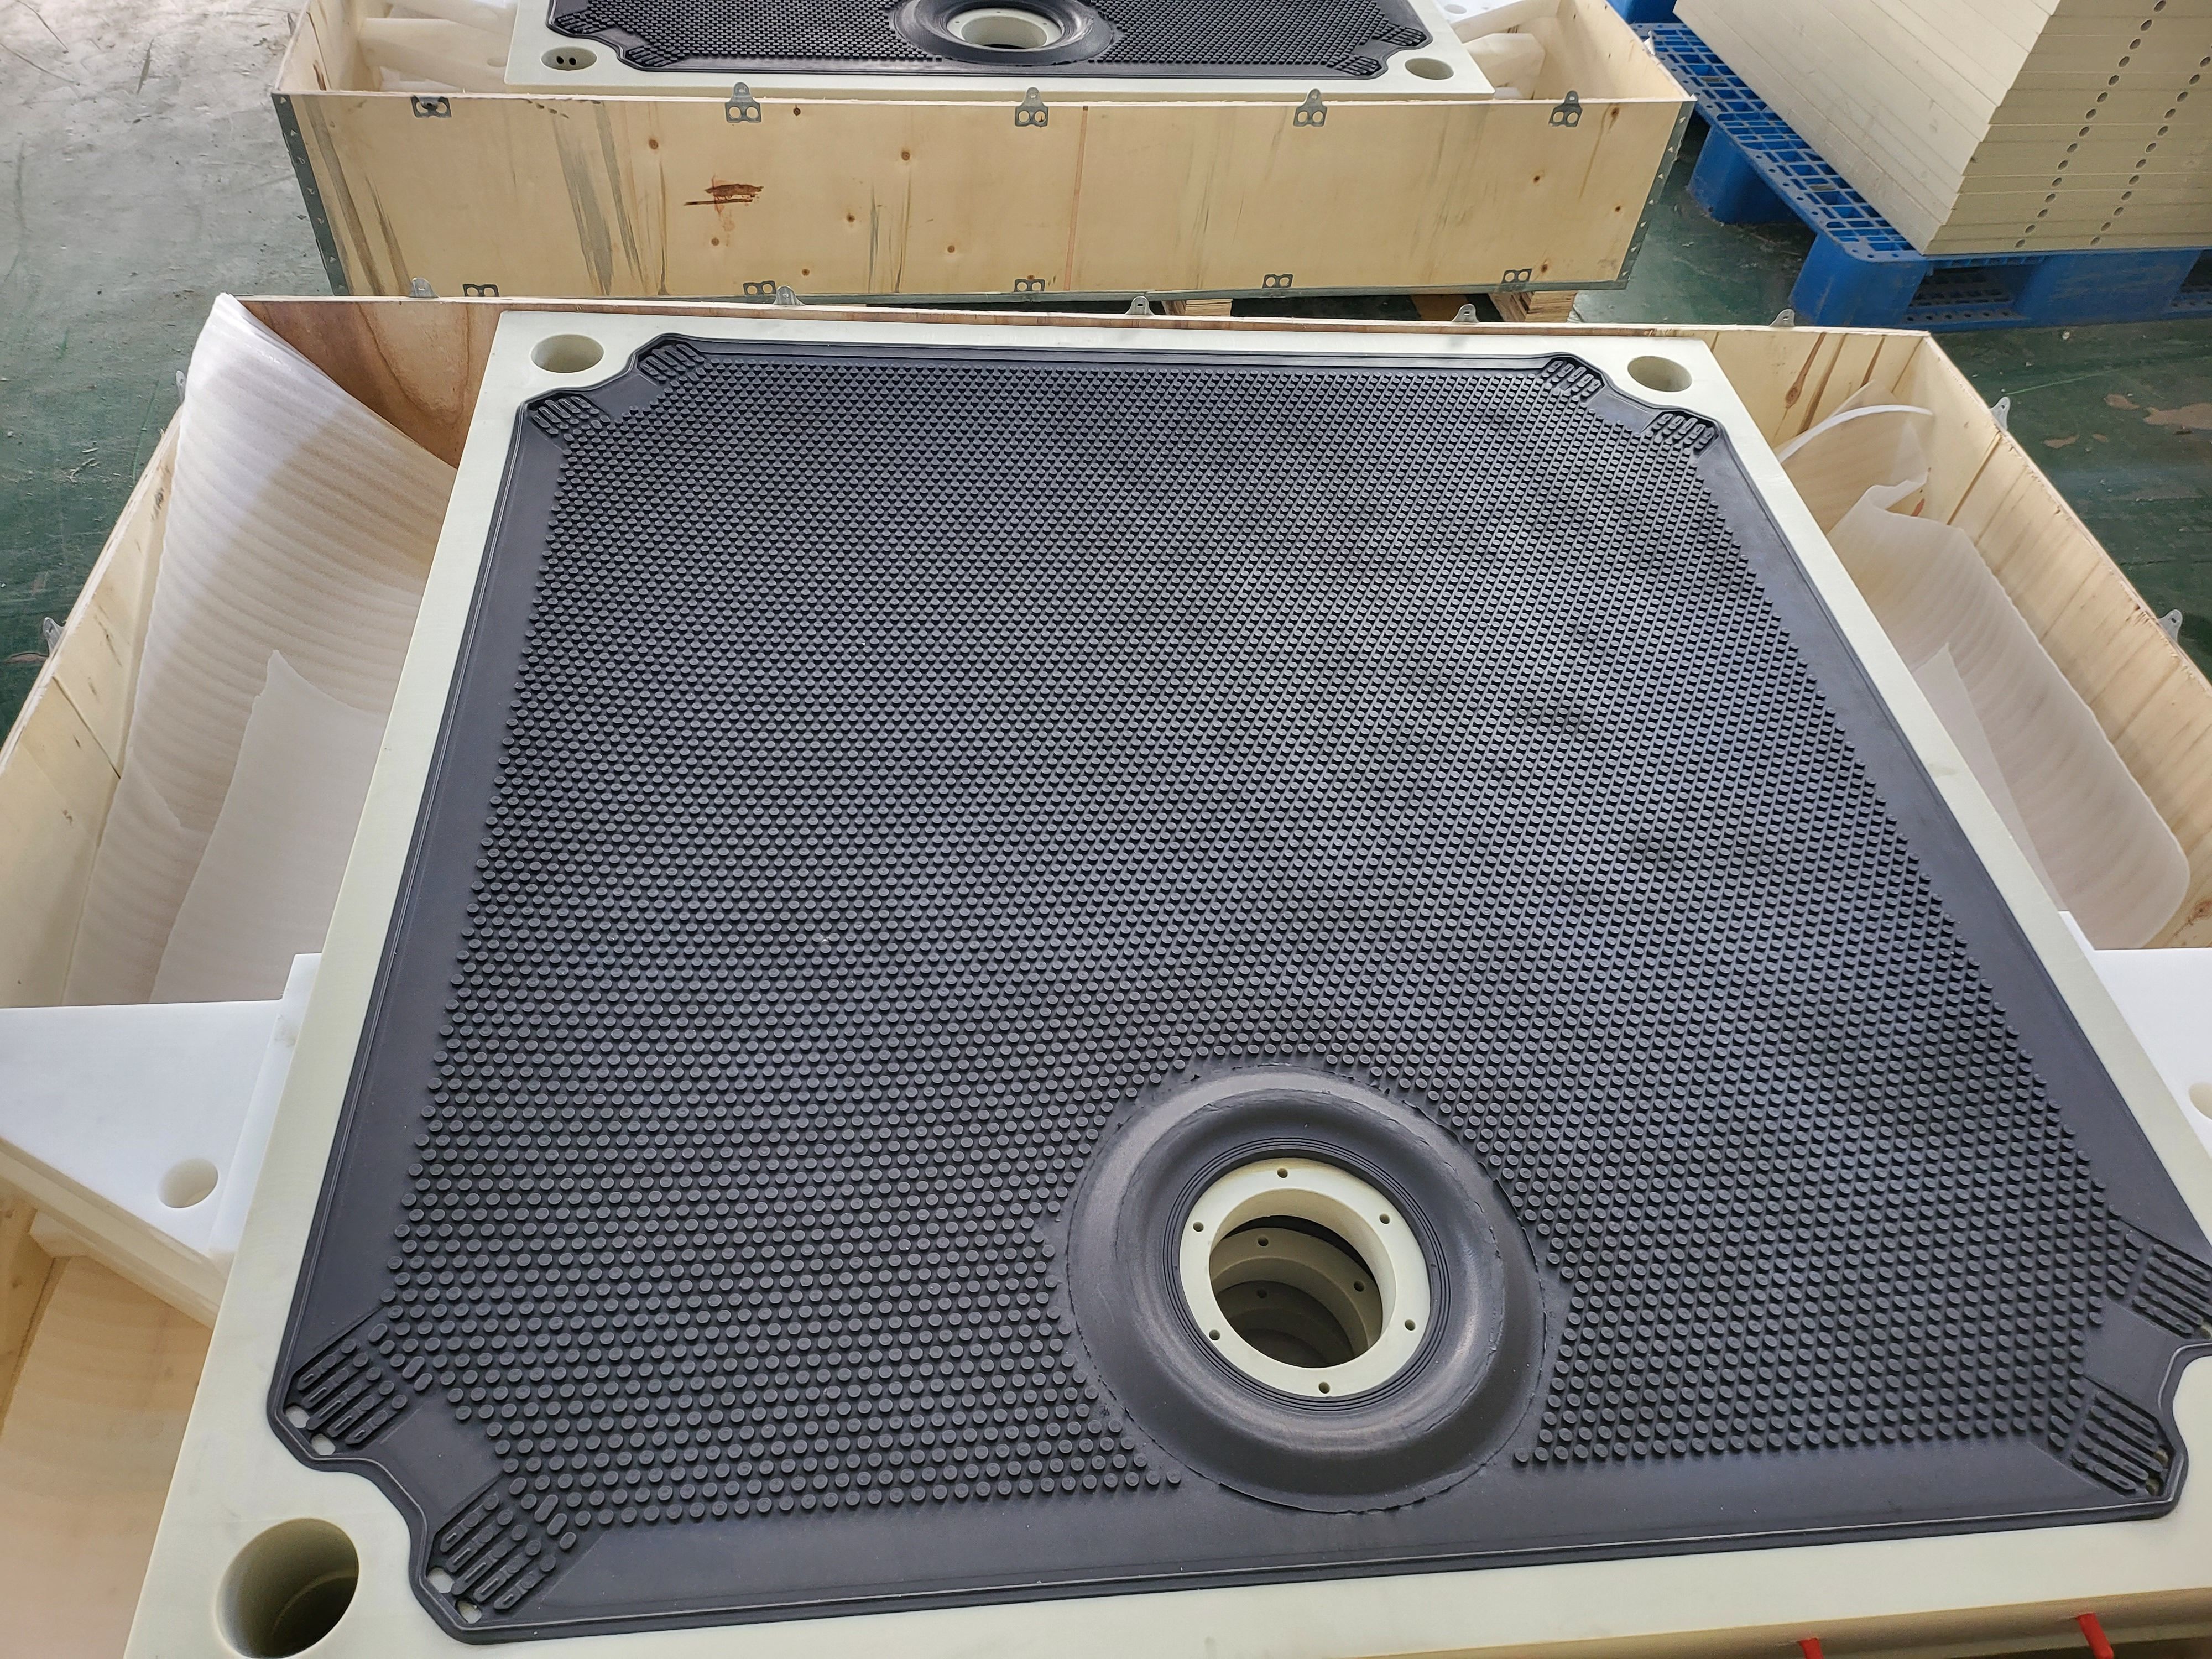
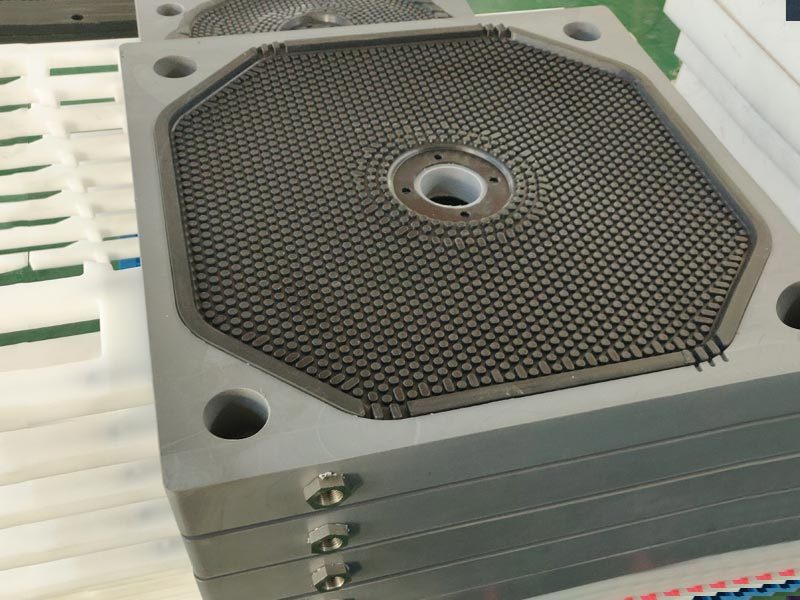
ProductMain products: vertical and horizontal imported and domestic filter plates, diaphragm plates, diaphragms and accessories; pinch valve sleeves and pinch valves and various mining accessories.
-
NewsIn 2013, our company's high-pressure cylinder with phenolic cloth support and guide ring obtained the national key new product certificate, project number: 2013GRA20011; its products in coal cylinders and engineering hydrauli
-
ServiceWe will actively cooperate with more enthusiasm, strengthen internal management, expand the market externally, improve various performance indicators of existing products, and truly achieve our win-win situation!
-
RecruitmentOur company always adheres to the talent concept of "people-oriented", provides a growth platform for talents, and realizes the common growth and development of enterprises and talents.


language
English
العربية
বাংলাদেশ
Български
Hrvatski
Česky
Dansk
Nederland
 Esperanto
Slovenski
Filipino
Suomi
Français
Maori
 Shqiptare
Georgian
 Euskara
Deutsch
Ελλάδα
ישראל
इंडिया
Magyarország
Ísland
Indonesia
Irlanda
Italia
日本語
Sovensko
Հայաստան
한국
Kyrgyz
ປະເທດລາວ
 Zulu
Latvian
Lithuanian
Luxembourgish
 Latinus
Macedonian
Малайская
Maltese
Монгол улс
 Cymraeg
ဗမာ
 தமிழ்
नेपाल
Norge
ایران
Polska
Portugal
România
Российская
Србија
 Slovak
Србија
 Slovak
Bosanski
Slovenian
Беларус
España
Sverige
Точик
ประเทศไทย
Türk
Azərbaycan
Uzbek
 Afrikaans
Việt Nam
Understanding Dust Rings: Importance and Applications in Industrial Sealing
Release time:
2025-04-26
Dust rings are specialized sealing components designed to prevent dust, dirt, and other contaminants from entering critical areas of machinery. In industrial environments, where equipment is often exposed to harsh conditions, the presence of dust and debris can lead to significant wear and tear, reduced efficiency, and increased maintenance costs. Therefore, understanding the role of dust rings ca
Dust rings are specialized sealing components designed to prevent dust, dirt, and other contaminants from entering critical areas of machinery. In industrial environments, where equipment is often exposed to harsh conditions, the presence of dust and debris can lead to significant wear and tear, reduced efficiency, and increased maintenance costs. Therefore, understanding the role of dust rings can be instrumental in ensuring the longevity and performance of industrial equipment.
One of the primary functions of a dust ring is to act as a barrier against particulate matter. When installed correctly, dust rings create a tight seal that prevents external contaminants from penetrating the machinery. This is particularly important in applications such as hydraulic systems, bearings, and rotating shafts, where even small amounts of dust can cause significant damage over time. By utilizing dust rings, industries can reduce the likelihood of mechanical failure and minimize downtime.
In addition to protecting against dust, dust rings can also help retain lubrication within the sealed area. This is crucial for components that rely on oil or grease for optimal functioning. By keeping lubricants contained, dust rings ensure that machinery operates smoothly and efficiently, thereby enhancing overall productivity.
Moreover, dust rings come in various materials and designs to suit different industrial applications. Depending on the specific requirements, these seals can be made from rubber, polyurethane, or other engineered materials, each offering unique properties such as flexibility, resistance to chemicals, and temperature tolerance. This versatility allows industries to select the most appropriate dust ring for their equipment, further optimizing performance.
Additionally, the installation of dust rings can lead to cost savings in the long run. By preventing contamination and maintaining lubrication, these seals help reduce maintenance frequency and extend the lifespan of critical components. This not only enhances operational efficiency but also lowers the total cost of ownership for equipment.
In summary, dust rings are essential for protecting industrial machinery from contaminants, ensuring efficient operation, and prolonging equipment life. By understanding the importance and applications of dust rings, industries can make informed decisions that enhance their operational reliability and minimize maintenance costs. Investing in quality sealing solutions, including dust rings, is a proactive approach that contributes to the smooth functioning of industrial equipment and ultimately drives business success.
Related News