-
AboutHebei Linaier Rubber Products Co., Ltd. is located in Duqiao Industrial Zone, Jingxian City, Hebei Province, adjacent to Dezhou, Shandong. Founded in early 2001 with a registered capital of 35 million yuan, it is a scientific

-
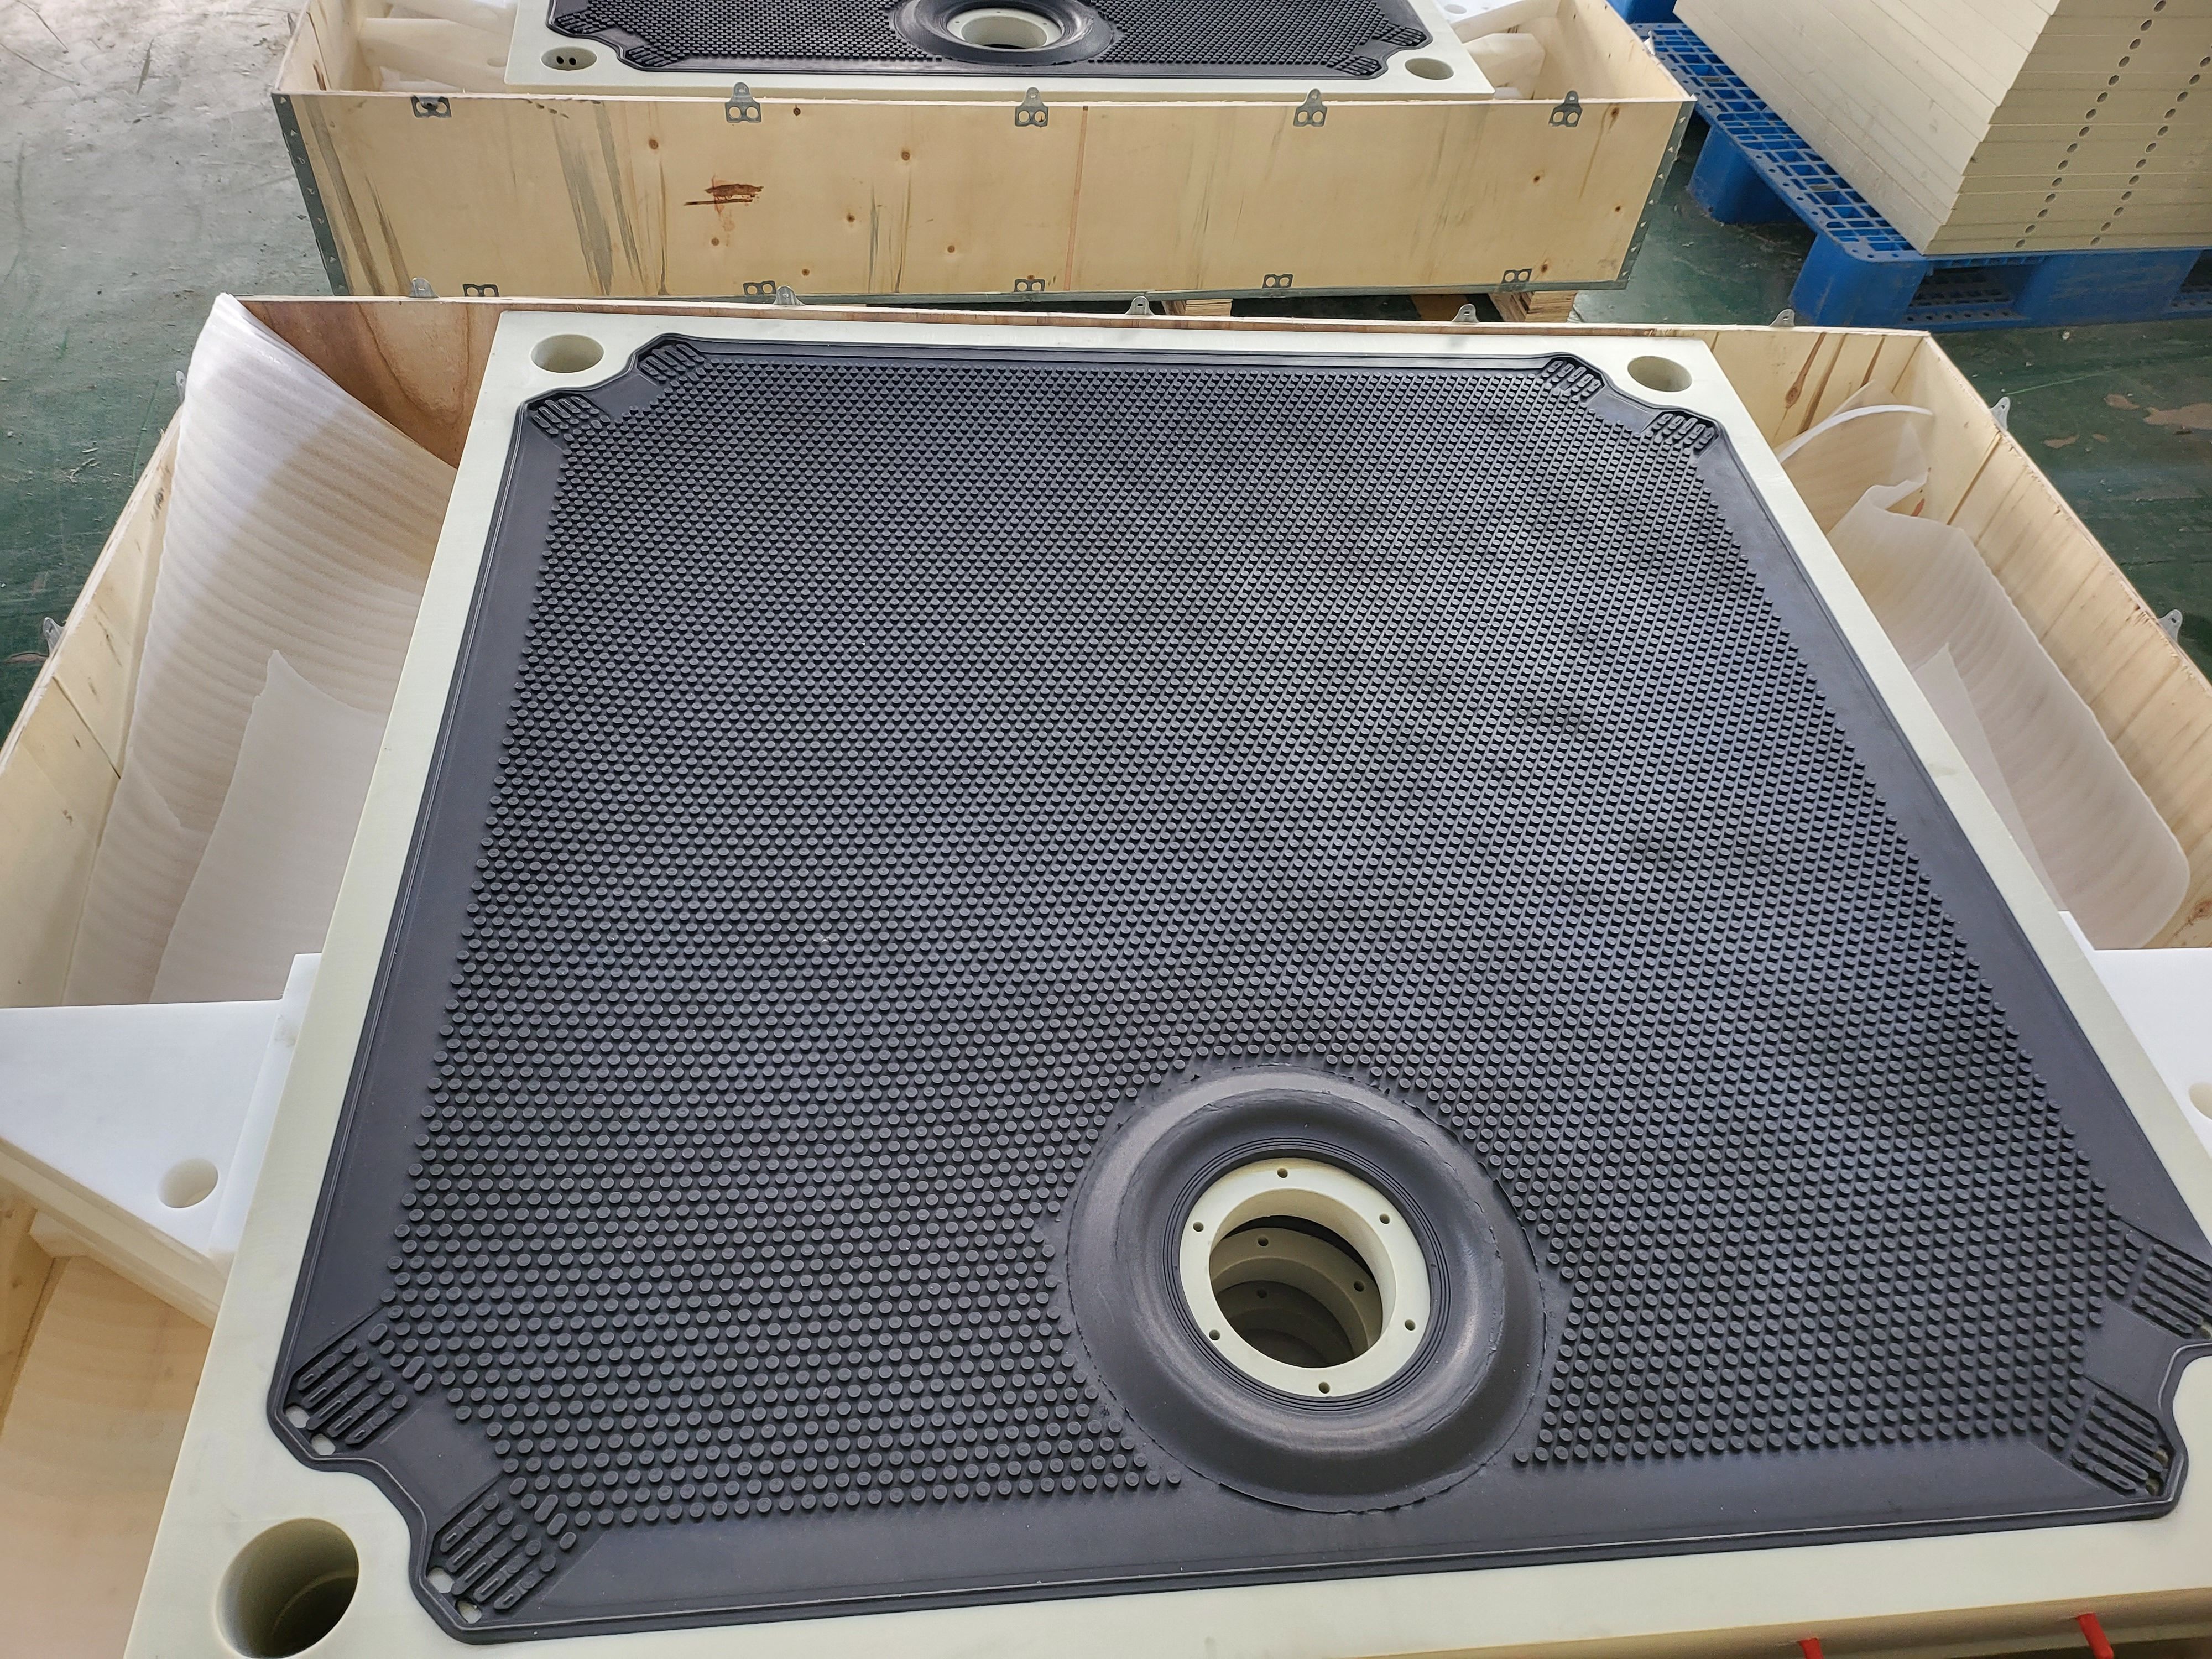
ProductMain products: vertical and horizontal imported and domestic filter plates, diaphragm plates, diaphragms and accessories; pinch valve sleeves and pinch valves and various mining accessories.
-
NewsIn 2013, our company's high-pressure cylinder with phenolic cloth support and guide ring obtained the national key new product certificate, project number: 2013GRA20011; its products in coal cylinders and engineering hydrauli
-
ServiceWe will actively cooperate with more enthusiasm, strengthen internal management, expand the market externally, improve various performance indicators of existing products, and truly achieve our win-win situation!
-
RecruitmentOur company always adheres to the talent concept of "people-oriented", provides a growth platform for talents, and realizes the common growth and development of enterprises and talents.


language
English
العربية
বাংলাদেশ
Български
Hrvatski
Česky
Dansk
Nederland
 Esperanto
Slovenski
Filipino
Suomi
Français
Maori
 Shqiptare
Georgian
 Euskara
Deutsch
Ελλάδα
ישראל
इंडिया
Magyarország
Ísland
Indonesia
Irlanda
Italia
日本語
Sovensko
Հայաստան
한국
Kyrgyz
ປະເທດລາວ
 Zulu
Latvian
Lithuanian
Luxembourgish
 Latinus
Macedonian
Малайская
Maltese
Монгол улс
 Cymraeg
ဗမာ
 தமிழ்
नेपाल
Norge
ایران
Polska
Portugal
România
Российская
Србија
 Slovak
Србија
 Slovak
Bosanski
Slovenian
Беларус
España
Sverige
Точик
ประเทศไทย
Türk
Azərbaycan
Uzbek
 Afrikaans
Việt Nam
Understanding the Critical Role of Sealing Rings in Industrial Equipment
Release time:
2025-03-06
Understanding the Critical Role of Sealing Rings in Industrial Equipment Table of Contents 1. Introduction to Sealing Rings in Industrial Applications 2. Types of Sealing Rings and Their Functions 2.1 O-Rings 2.2 V-Rings 2.3 U-Rings 3. Materials Used in Sealing Rings 4. Applications of Sealing Rings in Industrial Equipment
Understanding the Critical Role of Sealing Rings in Industrial Equipment
Table of Contents
- 1. Introduction to Sealing Rings in Industrial Applications
- 2. Types of Sealing Rings and Their Functions
- 3. Materials Used in Sealing Rings
- 4. Applications of Sealing Rings in Industrial Equipment
- 5. Proper Installation Techniques for Sealing Rings
- 6. Maintenance and Troubleshooting of Sealing Rings
- 7. Benefits of Using High-Quality Sealing Rings
- 8. Conclusion
- 9. Frequently Asked Questions (FAQs)
1. Introduction to Sealing Rings in Industrial Applications
In the realm of industrial equipment, **sealing rings** serve a pivotal role in ensuring operational efficiency and equipment longevity. These components, often overlooked, function as the first line of defense against leaks and contamination, thereby safeguarding the machinery they protect. As we delve into the various aspects of sealing rings, it becomes evident that their importance extends beyond mere functionality; they are crucial to the reliability and performance of industrial systems.
2. Types of Sealing Rings and Their Functions
Sealing rings come in various types, each designed to meet specific application needs. Understanding these types and their functions is essential for selecting the right sealing solution for your industrial equipment.
2.1 O-Rings
**O-rings** are one of the most widely used sealing devices in industrial applications. Characterized by their circular cross-section, these rings are utilized to form a seal between two mating surfaces. When compressed, O-rings create a tight seal that prevents fluid leakage and protects against contaminants. Their versatility makes them suitable for a broad range of applications, from hydraulic systems to automotive components.
2.2 V-Rings
**V-rings** are another type of sealing ring that offers unique advantages. They feature a V-shaped cross-section and are primarily used to seal rotating shafts. Unlike O-rings, V-rings can accommodate angular misalignment and are resistant to wear, making them ideal for dynamic applications. These rings effectively keep dirt and moisture away from the shaft, enhancing the longevity of the machinery.
2.3 U-Rings
**U-rings**, or U-cup seals, are designed to provide superior sealing performance in applications involving linear motion. Their U-shaped cross-section allows for effective sealing against pressure from either direction, making them highly efficient for hydraulic and pneumatic applications. U-rings are particularly useful in cylinders where fluid pressure can vary significantly.
3. Materials Used in Sealing Rings
The performance of sealing rings heavily relies on the materials from which they are made. Various materials offer different properties, making them suitable for specific applications.
3.1 Rubber
**Rubber** is a common material used for O-rings and seals due to its flexibility and resilience. It can withstand moderate temperatures and pressures, making it ideal for a variety of industrial applications. However, rubber may degrade over time when exposed to certain chemicals or extreme temperatures.
3.2 PTFE (Polytetrafluoroethylene)
**PTFE**, also known as Teflon, is renowned for its chemical resistance and low friction properties. Sealing rings made of PTFE are suitable for high-temperature and high-pressure applications, such as in the chemical processing industry. Their durability ensures a long service life, reducing the need for frequent replacements.
3.3 Silicone
**Silicone** sealing rings are favored in applications requiring high flexibility and temperature resistance. They maintain their sealing capabilities in extreme conditions, making them ideal for food and pharmaceutical industries where contamination must be avoided.
4. Applications of Sealing Rings in Industrial Equipment
Sealing rings are employed across a multitude of industries, playing a crucial role in various applications.
4.1 Automotive Industry
In the automotive sector, sealing rings are essential components in engines, transmissions, and braking systems. They ensure fluid containment, preventing leaks that could compromise vehicle performance and safety.
4.2 Hydraulic and Pneumatic Systems
Hydraulic and pneumatic systems rely heavily on sealing rings to maintain pressure and prevent leaks. Proper sealing is critical for the efficient operation of these systems, as even minor leaks can lead to significant performance losses.
4.3 Chemical Processing
In chemical processing plants, sealing rings made of materials like PTFE are crucial for containing corrosive substances. These seals prevent contamination and protect equipment from harsh chemicals, ensuring the integrity of the manufacturing process.
4.4 Food and Beverage Industry
The food and beverage industry requires sealing solutions that meet stringent hygiene standards. Silicone and other food-safe materials are commonly used for sealing rings in this sector, ensuring the safety and quality of consumable products.
5. Proper Installation Techniques for Sealing Rings
Correct installation of sealing rings is essential for optimal performance. Here are key techniques to ensure effective sealing:
5.1 Surface Preparation
Before installation, surfaces must be cleaned and free from dirt, debris, or old sealant. Any imperfections can lead to leakage or seal failure.
5.2 Correct Alignment
Ensure that the sealing ring is properly aligned with the mating surfaces. Misalignment can result in uneven compression and compromise sealing effectiveness.
5.3 Compression Guidelines
Follow manufacturer guidelines for compression. Over-compressing a sealing ring can cause damage, while under-compressing may lead to leaks.
6. Maintenance and Troubleshooting of Sealing Rings
Regular maintenance and troubleshooting can extend the life of sealing rings and prevent costly downtime.
6.1 Inspection
Routine inspections should be conducted to check for signs of wear, such as cracking, deformation, or discoloration. Early detection can prevent catastrophic failures.
6.2 Replacement Guidelines
Follow recommended replacement intervals based on operating conditions. Harsh environments may necessitate more frequent replacements.
6.3 Troubleshooting Common Issues
If leaks occur, investigate potential causes such as improper installation, material fatigue, or damage from contaminants. Addressing these issues promptly is crucial to maintaining equipment performance.
7. Benefits of Using High-Quality Sealing Rings
Investing in high-quality sealing rings offers numerous advantages that can significantly enhance operational efficiency.
7.1 Improved Reliability
High-quality sealing rings provide enhanced reliability, reducing the likelihood of leaks and equipment failures. This reliability contributes to overall operational efficiency.
7.2 Cost Savings
By preventing leaks and reducing the need for frequent replacements, high-quality sealing rings can lead to significant cost savings in maintenance and downtime.
7.3 Enhanced Performance
Sealing rings designed with advanced materials and engineering can improve the overall performance of industrial equipment, allowing for better precision and efficiency.
8. Conclusion
Sealing rings are indispensable components in industrial equipment, playing a vital role in ensuring operational efficiency and equipment longevity. Understanding the various types, materials, and applications of sealing rings is crucial for selecting the right solutions for specific industrial needs. By investing in high-quality sealing rings and adhering to proper installation and maintenance practices, industries can achieve remarkable improvements in performance and reliability.
9. Frequently Asked Questions (FAQs)
1. What are the main functions of sealing rings?
Sealing rings primarily serve to prevent fluid leaks and protect against contaminants in industrial equipment. They ensure the integrity of systems involving hydraulic, pneumatic, and chemical processes.
2. How do I choose the right sealing ring for my application?
Selecting the appropriate sealing ring involves considering factors such as the type of fluid, pressure, temperature, and compatibility with materials. Consulting with manufacturers or industry experts can aid in making the right decision.
3. What maintenance practices should I follow for sealing rings?
Regular inspections for wear, proper alignment, and adherence to replacement intervals are crucial for maintaining sealing rings. It is essential to address any signs of damage promptly to prevent leaks.
4. Can sealing rings be reused?
In general, sealing rings are not designed for reuse, especially if they show signs of wear or deformation. Replacing them with new ones is recommended for optimal performance.
5. What materials are commonly used for sealing rings?
Common materials include rubber, PTFE (Teflon), and silicone, each offering unique properties suited for specific applications. Selecting the right material is critical for ensuring performance under varying conditions.
Related News