-
AboutHebei Linaier Rubber Products Co., Ltd. is located in Duqiao Industrial Zone, Jingxian City, Hebei Province, adjacent to Dezhou, Shandong. Founded in early 2001 with a registered capital of 35 million yuan, it is a scientific

-
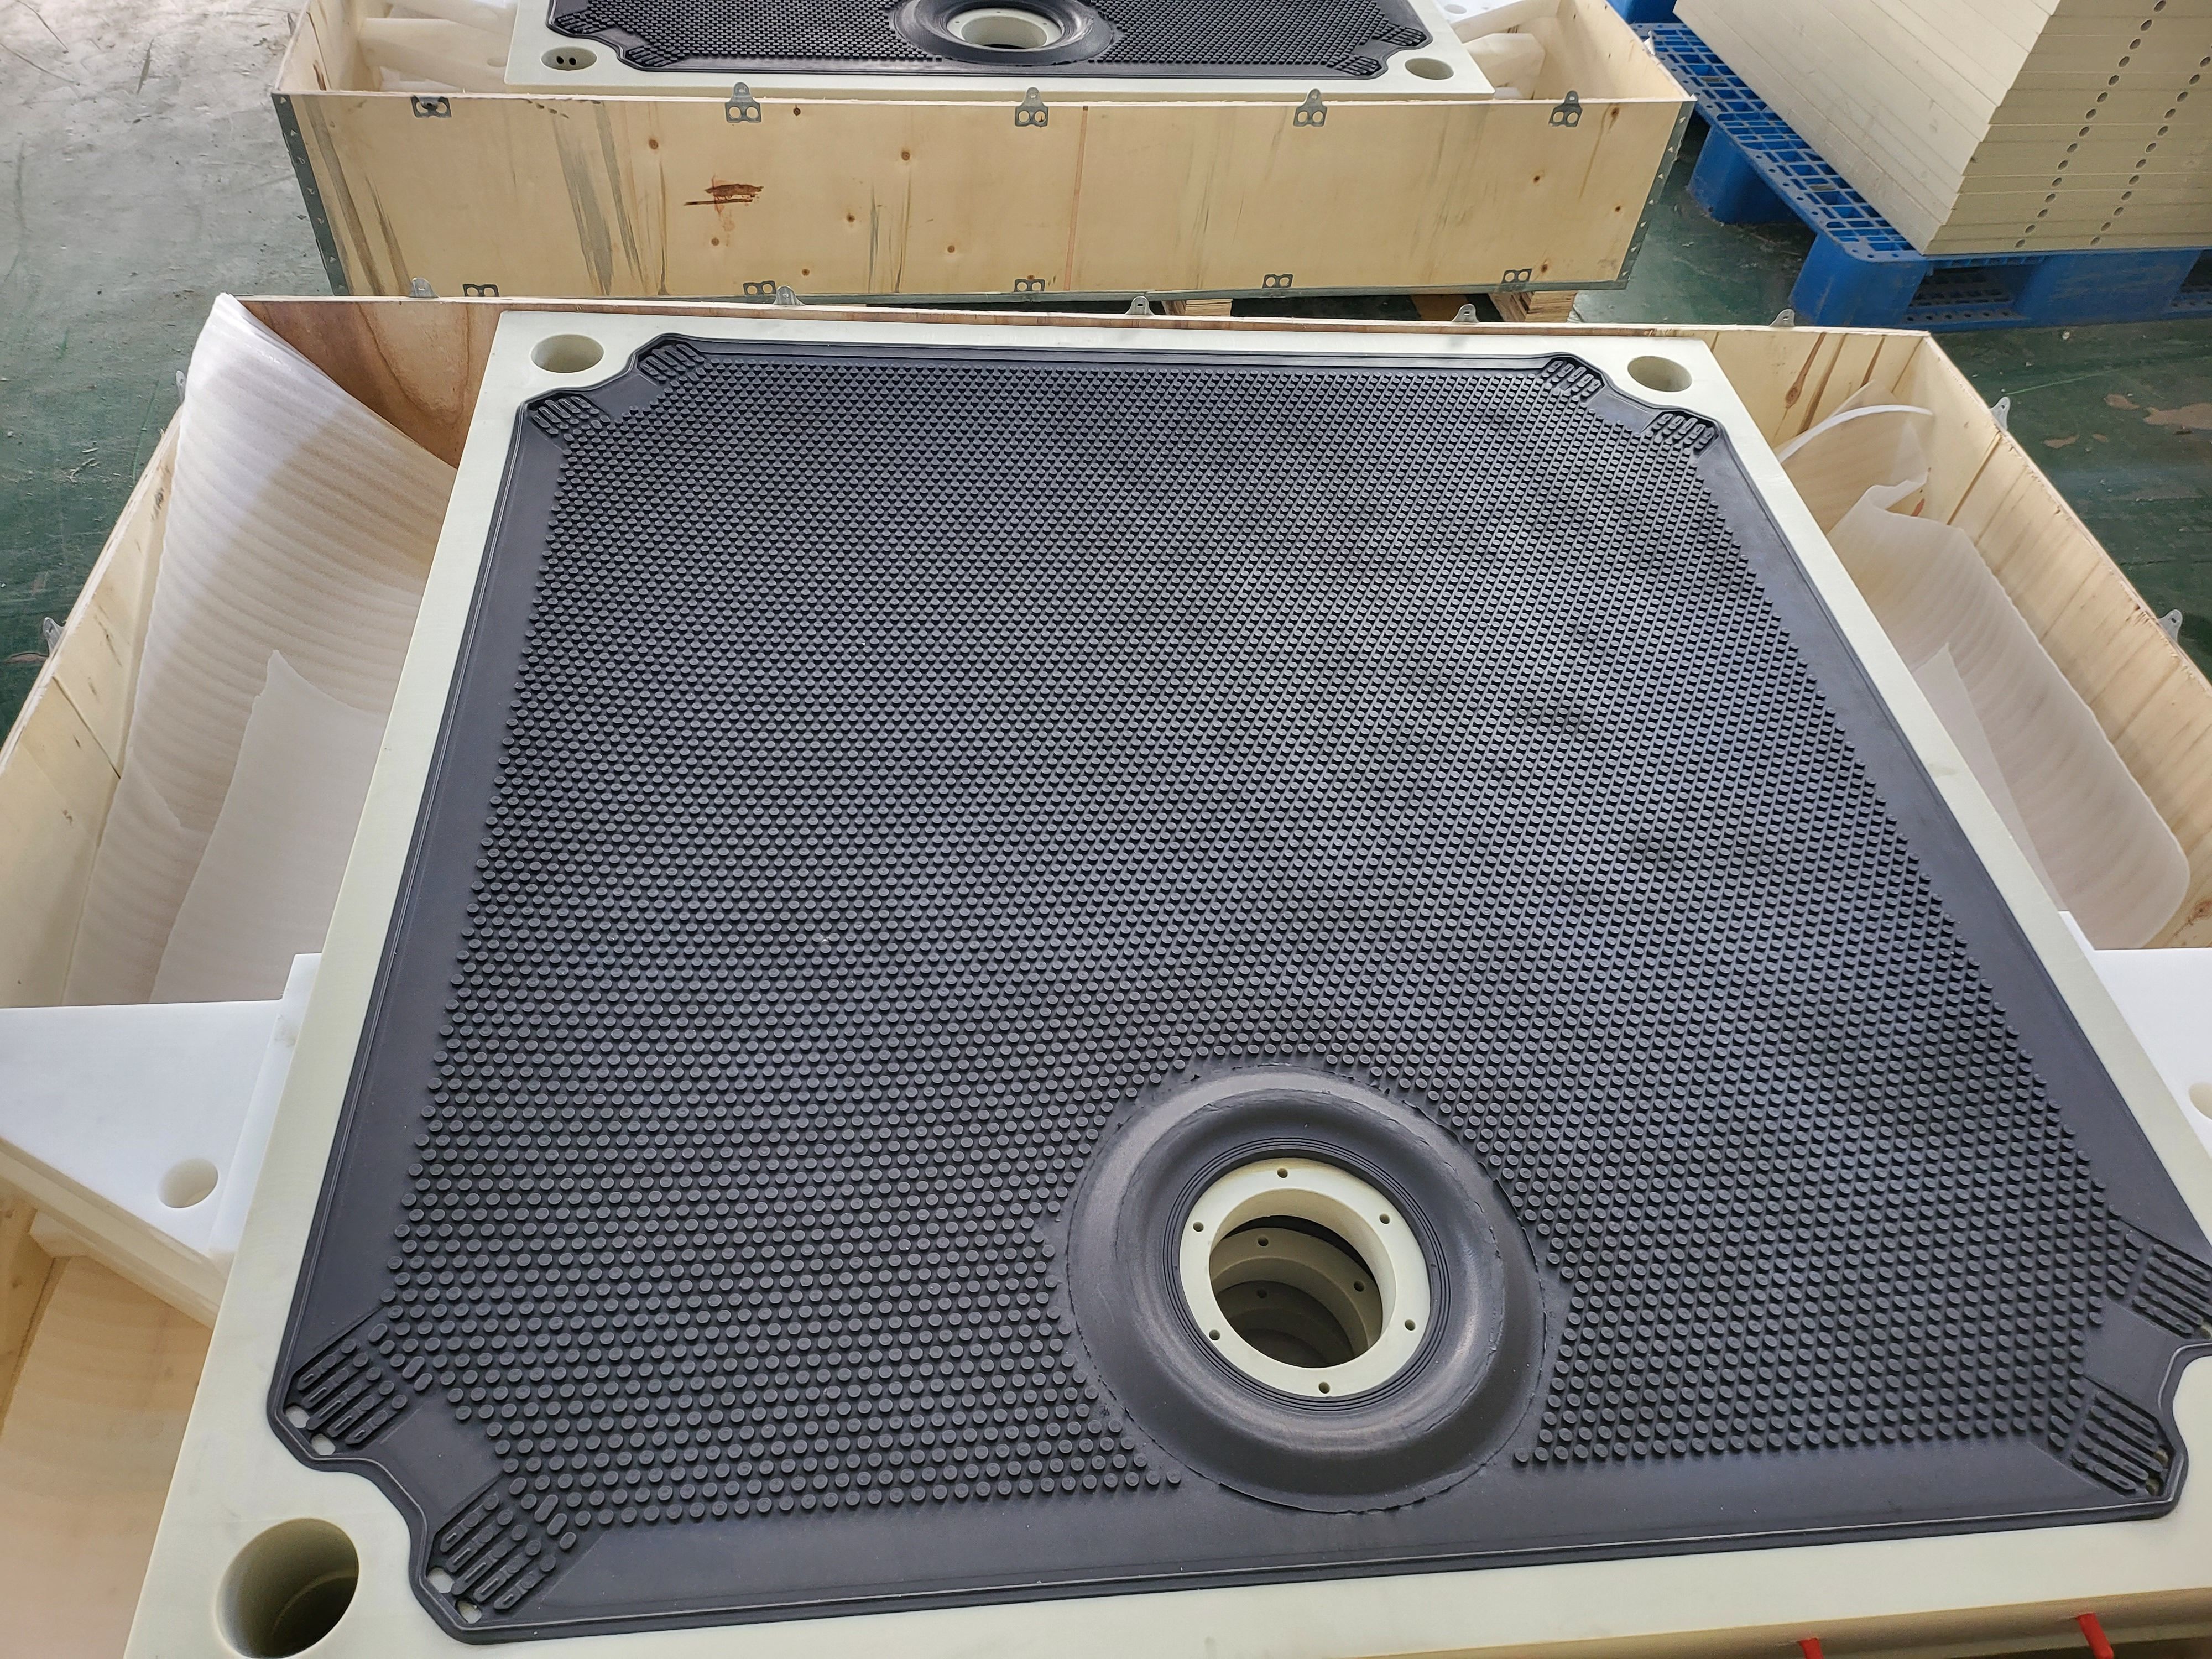
ProductMain products: vertical and horizontal imported and domestic filter plates, diaphragm plates, diaphragms and accessories; pinch valve sleeves and pinch valves and various mining accessories.
-
NewsIn 2013, our company's high-pressure cylinder with phenolic cloth support and guide ring obtained the national key new product certificate, project number: 2013GRA20011; its products in coal cylinders and engineering hydrauli
-
ServiceWe will actively cooperate with more enthusiasm, strengthen internal management, expand the market externally, improve various performance indicators of existing products, and truly achieve our win-win situation!
-
RecruitmentOur company always adheres to the talent concept of "people-oriented", provides a growth platform for talents, and realizes the common growth and development of enterprises and talents.


language
English
العربية
বাংলাদেশ
Български
Hrvatski
Česky
Dansk
Nederland
 Esperanto
Slovenski
Filipino
Suomi
Français
Maori
 Shqiptare
Georgian
 Euskara
Deutsch
Ελλάδα
ישראל
इंडिया
Magyarország
Ísland
Indonesia
Irlanda
Italia
日本語
Sovensko
Հայաստան
한국
Kyrgyz
ປະເທດລາວ
 Zulu
Latvian
Lithuanian
Luxembourgish
 Latinus
Macedonian
Малайская
Maltese
Монгол улс
 Cymraeg
ဗမာ
 தமிழ்
नेपाल
Norge
ایران
Polska
Portugal
România
Российская
Србија
 Slovak
Србија
 Slovak
Bosanski
Slovenian
Беларус
España
Sverige
Точик
ประเทศไทย
Türk
Azərbaycan
Uzbek
 Afrikaans
Việt Nam
Exploring the Versatility of Pinch Valve Series in Chemical Manufacturing
Release time:
2023-09-18
Table of Contents: 1. Introduction: Pinch Valves in Chemical Manufacturing 2. Understanding Pinch Valve Series 3. Applications and Benefits in Chemical Manufacturing 4. Advanced Features and Innovations of Pinch Valves 5. Considerations for Choosing Pinch Valve Series 6. Frequently Asked Questions (FAQs) 7. Conclusion **1. Introduction: Pinch Valves in Chemical Manufacturing** In the dynamic field
Table of Contents:
1. Introduction: Pinch Valves in Chemical Manufacturing
2. Understanding Pinch Valve Series
3. Applications and Benefits in Chemical Manufacturing
4. Advanced Features and Innovations of Pinch Valves
5. Considerations for Choosing Pinch Valve Series
6. Frequently Asked Questions (FAQs)
7. Conclusion
**1. Introduction: Pinch Valves in Chemical Manufacturing**
In the dynamic field of chemical manufacturing, the need for precise control and reliable flow of chemicals is paramount. This is where pinch valve series come into play. These versatile valve systems offer a range of benefits that ensure smooth processes and optimal performance. From regulating the flow rate to preventing leakage and contamination, pinch valves are essential components for various applications in the chemical industry.
**2. Understanding Pinch Valve Series**
Pinch valves are uniquely designed to control the flow of fluids by pinching or compressing a flexible tube. This mechanism allows for quick and efficient shut-off, offering superior control over the fluid flow. The pinch valve series comprises a wide range of models, each tailored to specific requirements and applications.
**3. Applications and Benefits in Chemical Manufacturing**
Pinch valve series find numerous applications in chemical manufacturing processes. They are extensively used in:
- Chemical dosing and metering: Pinch valves ensure accurate and precise dosing of chemicals, facilitating efficient mixing and reaction processes.
- Slurry and abrasive fluid handling: The robust construction of pinch valves allows them to handle abrasive slurries without clogging or damage. This makes them ideal for transporting and controlling the flow of highly abrasive chemicals.
- Chemical dispensing and filling: Pinch valves offer precise control over the dispensing and filling of chemicals, ensuring accurate measurements and preventing spillage or wastage.
- Controlling corrosive fluids: Pinch valves are resistant to corrosion, making them suitable for handling highly corrosive chemicals without compromising their durability or performance.
The benefits of using pinch valve series in chemical manufacturing include:
- Accurate flow control: Pinch valves provide precise control over the flow rate, allowing operators to maintain optimal process conditions.
- Easy maintenance and cleaning: The simple and accessible design of pinch valves enables easy maintenance and cleaning, minimizing downtime and maximizing productivity.
- Leak-proof operation: Pinch valves offer a tight seal, preventing leakage and minimizing the risk of contamination in chemical processes.
**4. Advanced Features and Innovations of Pinch Valves**
Pinch valve series have evolved with advancements in technology, incorporating innovative features to enhance their performance and reliability. Some of the notable advancements include:
- Remote control and automation: Pinch valves can be integrated into automated systems, allowing for remote control and monitoring. This streamlines operations, improves efficiency, and reduces manual intervention.
- Smart sensors and feedback mechanisms: With the integration of smart sensors, pinch valves can provide real-time feedback on flow rates, pressure, and other crucial parameters. This enables operators to accurately monitor and optimize the manufacturing processes.
- Enhanced materials and coatings: Manufacturers now offer pinch valves with specialized materials and coatings, ensuring compatibility with aggressive chemicals and extending their lifespan in harsh environments.
**5. Considerations for Choosing Pinch Valve Series**
When selecting pinch valve series for chemical manufacturing applications, several factors should be considered:
- Chemical compatibility: Ensure that the materials used in the pinch valve are compatible with the chemicals being handled to prevent corrosion or chemical reactions.
- Pressure and temperature requirements: Assess the operating conditions and select pinch valves with suitable pressure and temperature ratings to ensure optimal performance and durability.
- Valve size and flow capacity: Consider the desired flow rate and select pinch valves with appropriate sizes and flow capacities to meet the process requirements.
- Maintenance and serviceability: Evaluate the ease of maintenance and availability of spare parts when choosing pinch valve series. Opt for valves that offer easy access for maintenance and quick replacement of components.
**6. Frequently Asked Questions (FAQs)**
Q1: Can pinch valves handle corrosive chemicals?
Q2: Are pinch valves suitable for high-pressure applications?
Q3: How often should pinch valves be inspected and maintained?
Q4: Can pinch valves be integrated into automated systems?
Q5: What are the advantages of pinch valves over other valve types in chemical manufacturing?
**7. Conclusion**
Pinch valve series have proven to be indispensable in the world of chemical manufacturing. Their versatility, precise control, and robust construction make them ideal for various applications. From metering and dosing to handling corrosive fluids, pinch valves offer unmatched performance and reliability. As technology continues to advance, pinch valves are evolving to meet the ever-changing demands of the chemical industry. Embrace the versatility of pinch valve series and optimize your chemical manufacturing processes for enhanced productivity and efficiency.
Related News