-
AboutHebei Linaier Rubber Products Co., Ltd. is located in Duqiao Industrial Zone, Jingxian City, Hebei Province, adjacent to Dezhou, Shandong. Founded in early 2001 with a registered capital of 35 million yuan, it is a scientific

-
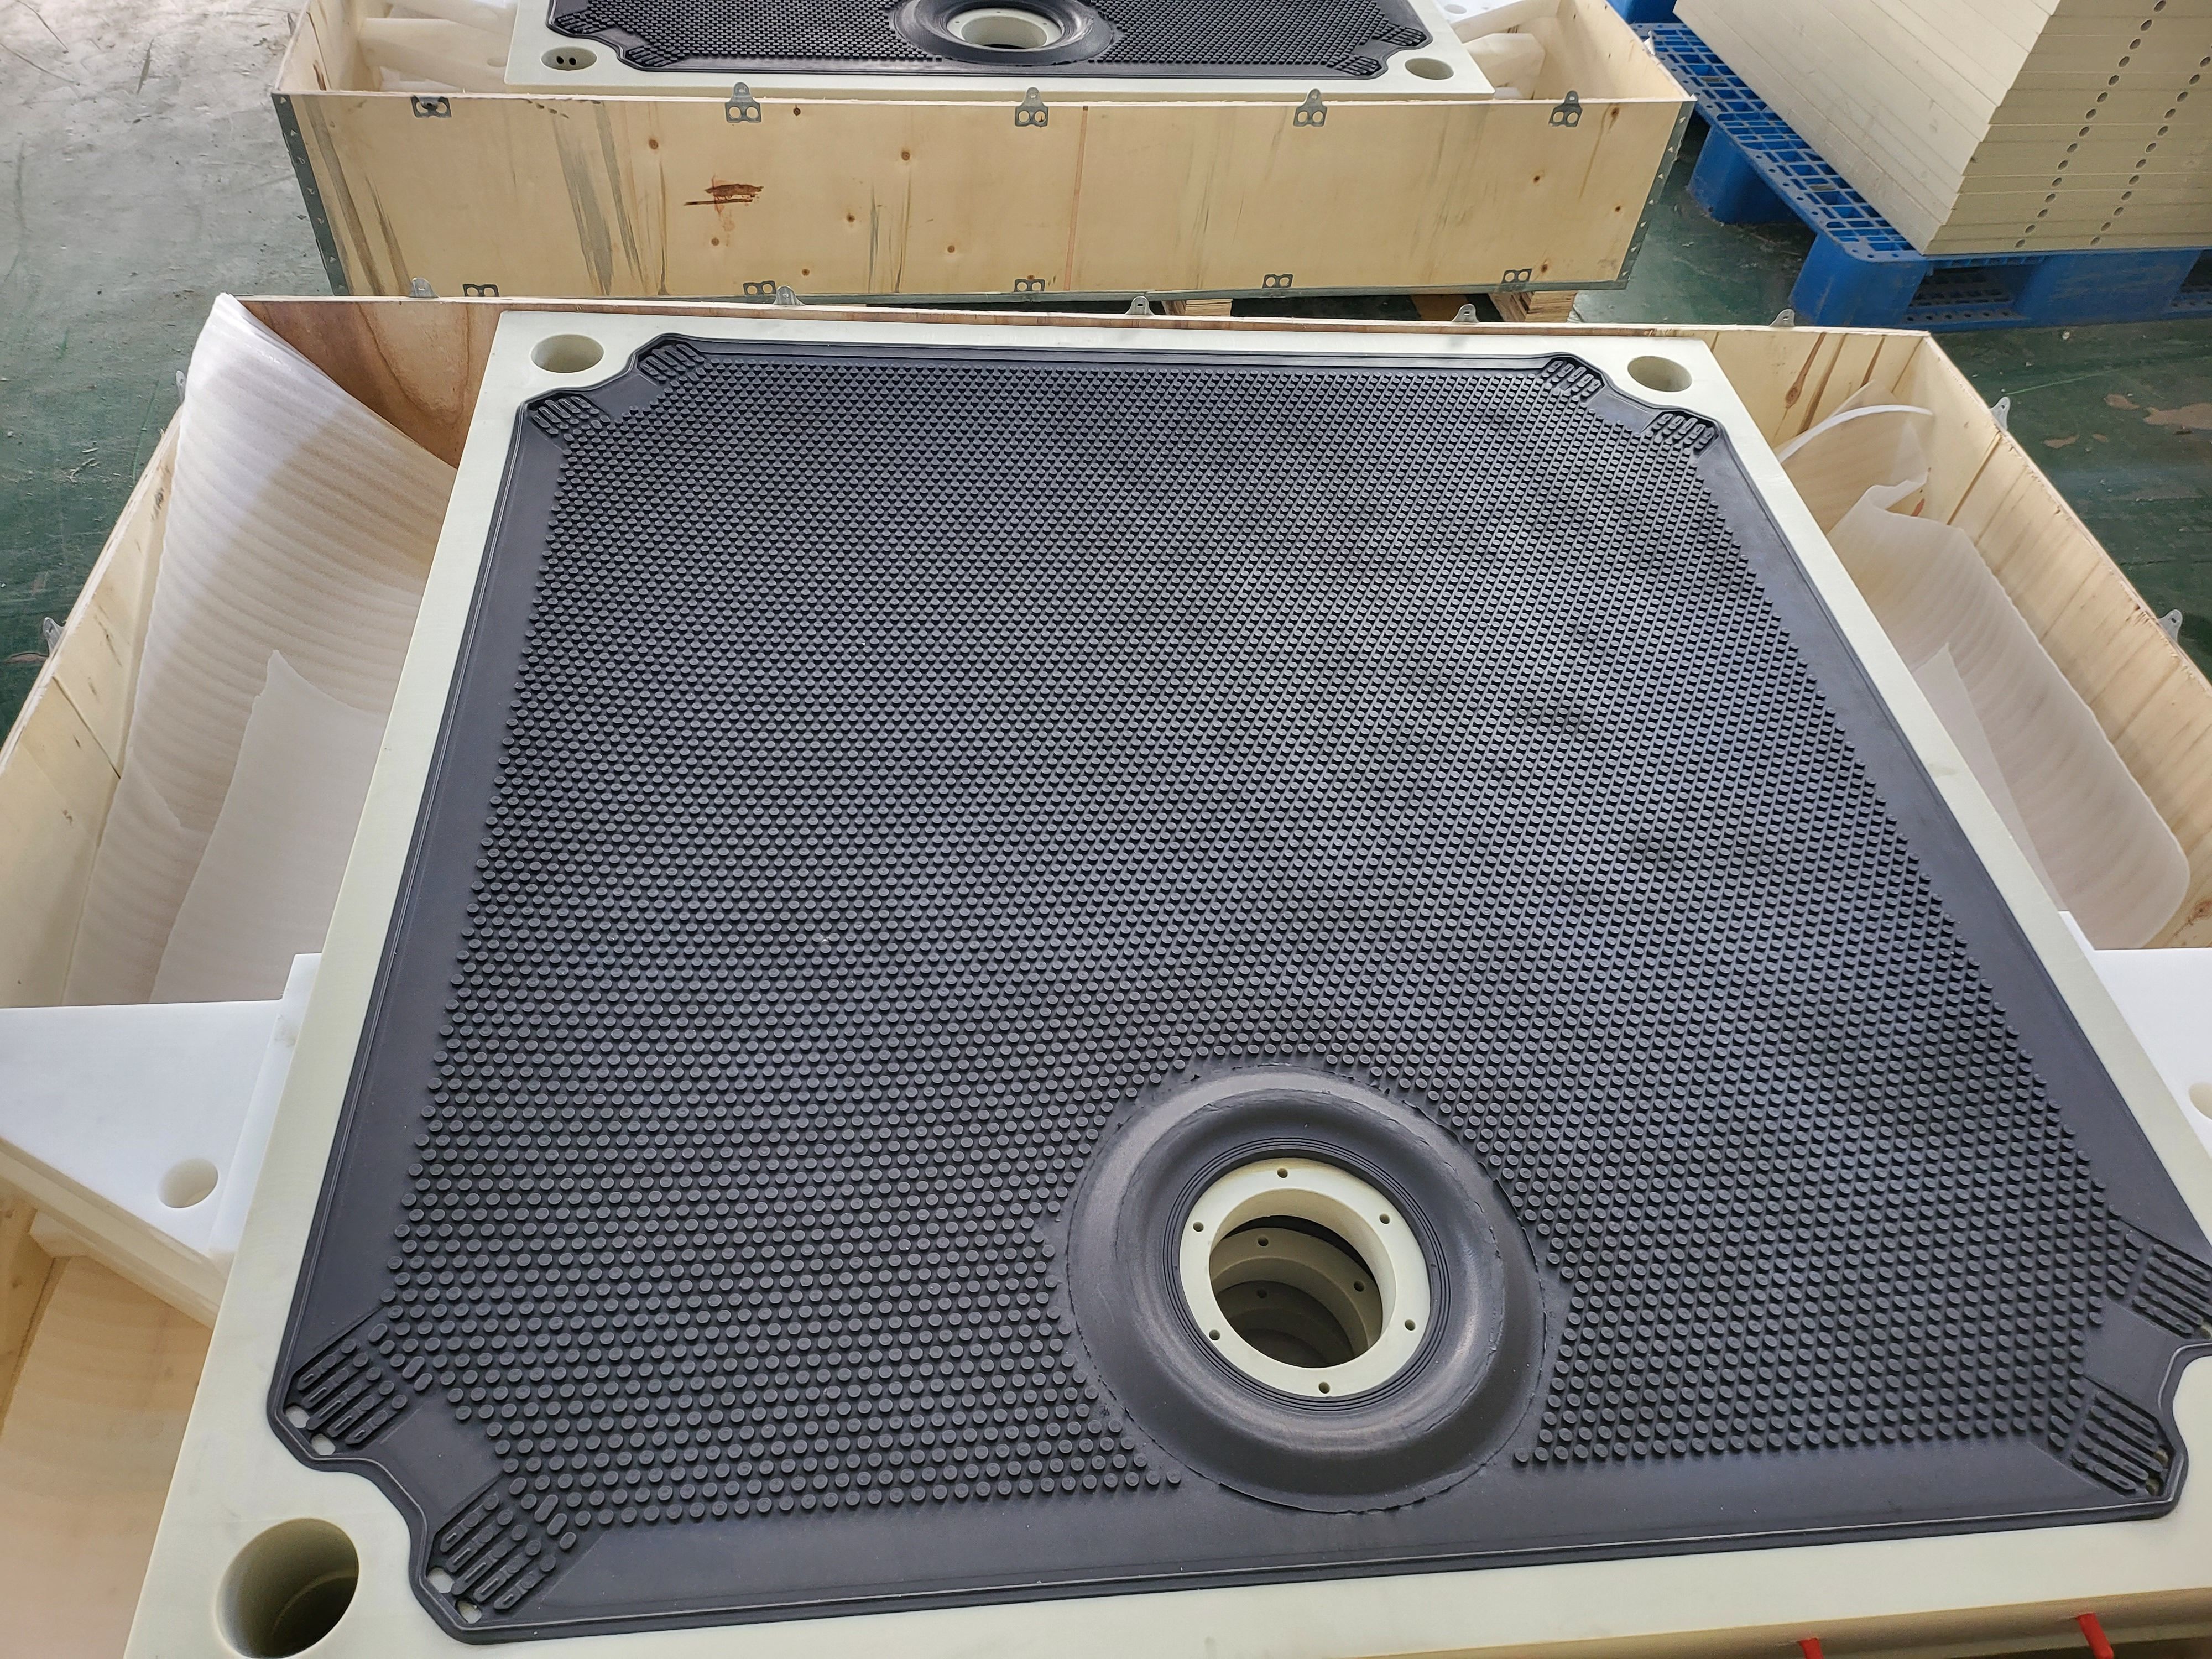
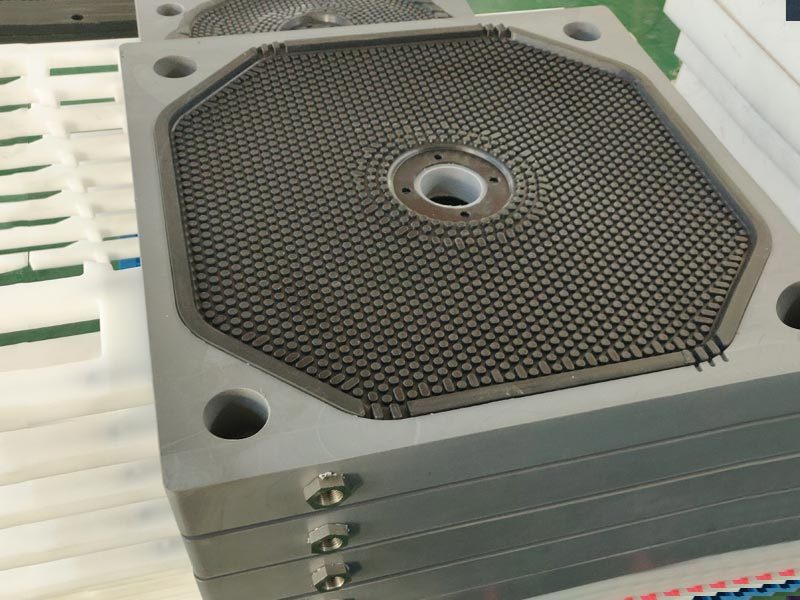
ProductMain products: vertical and horizontal imported and domestic filter plates, diaphragm plates, diaphragms and accessories; pinch valve sleeves and pinch valves and various mining accessories.
-
NewsIn 2013, our company's high-pressure cylinder with phenolic cloth support and guide ring obtained the national key new product certificate, project number: 2013GRA20011; its products in coal cylinders and engineering hydrauli
-
ServiceWe will actively cooperate with more enthusiasm, strengthen internal management, expand the market externally, improve various performance indicators of existing products, and truly achieve our win-win situation!
-
RecruitmentOur company always adheres to the talent concept of "people-oriented", provides a growth platform for talents, and realizes the common growth and development of enterprises and talents.


language
English
العربية
বাংলাদেশ
Български
Hrvatski
Česky
Dansk
Nederland
 Esperanto
Slovenski
Filipino
Suomi
Français
Maori
 Shqiptare
Georgian
 Euskara
Deutsch
Ελλάδα
ישראל
इंडिया
Magyarország
Ísland
Indonesia
Irlanda
Italia
日本語
Sovensko
Հայաստան
한국
Kyrgyz
ປະເທດລາວ
 Zulu
Latvian
Lithuanian
Luxembourgish
 Latinus
Macedonian
Малайская
Maltese
Монгол улс
 Cymraeg
ဗမာ
 தமிழ்
नेपाल
Norge
ایران
Polska
Portugal
România
Российская
Србија
 Slovak
Србија
 Slovak
Bosanski
Slovenian
Беларус
España
Sverige
Точик
ประเทศไทย
Türk
Azərbaycan
Uzbek
 Afrikaans
Việt Nam
The Importance of Sealing Rings in the Chemical Industry
Release time:
2023-09-11
Table of Contents: 1. Introduction: Understanding the Significance of Sealing Rings in the Chemical Industry 2. Types of Sealing Rings Used in the Chemical Industry 2.1. O-Rings 2.2. Gaskets 2.3. Metal Rings 2.4. Lip Seals 3. Applications of Sealing Rings in the Chemical Industry 3.1. Pumps and Compressors 3.2. Valves and Fittings 3.3. Reactors and Distillation Columns
Table of Contents:
1. Introduction: Understanding the Significance of Sealing Rings in the Chemical Industry
2. Types of Sealing Rings Used in the Chemical Industry
2.1. O-Rings
2.2. Gaskets
2.3. Metal Rings
2.4. Lip Seals
3. Applications of Sealing Rings in the Chemical Industry
3.1. Pumps and Compressors
3.2. Valves and Fittings
3.3. Reactors and Distillation Columns
3.4. Tanks and Pipelines
4. The Benefits of Using Sealing Rings in the Chemical Industry
4.1. Ensuring Safety and Preventing Leakage
4.2. Enhancing Equipment Performance and Efficiency
4.3. Minimizing Downtime and Maintenance Costs
4.4. Complying with Industry Regulations and Standards
5. Frequently Asked Questions (FAQs) about Sealing Rings in the Chemical Industry
5.1. What are the main factors to consider when selecting sealing rings for chemical applications?
5.2. How often should sealing rings be inspected and replaced?
5.3. Can sealing rings withstand extreme temperatures and corrosive chemicals?
5.4. Are there any specific installation or maintenance requirements for sealing rings?
5.5. Can sealing rings be customized for unique chemical industry needs?
6. Conclusion
1. Introduction: Understanding the Significance of Sealing Rings in the Chemical Industry
In the chemical industry, where hazardous substances, high pressures, and extreme temperatures are common, sealing rings play a crucial role in maintaining safety, ensuring efficiency, and preventing costly leaks. These vital components provide a reliable barrier between different parts of equipment, preventing the escape of fluids or gases and keeping contaminants out.
2. Types of Sealing Rings Used in the Chemical Industry
2.1. O-Rings
O-rings are one of the most commonly used sealing rings in the chemical industry. They are circular rubber or elastomer rings designed to fit into a groove and create a seal between two mating surfaces. O-rings offer excellent resistance to chemicals, high pressures, and temperature variations, making them suitable for various applications.
2.2. Gaskets
Gaskets are flat sealing rings typically made from materials such as rubber, metal, or composite. They are used to create a seal between two or more mating surfaces, preventing leakage. Gaskets are available in different shapes and sizes and are chosen based on the specific requirements of the equipment and chemicals involved.
2.3. Metal Rings
Metal rings, such as spiral wound gaskets or metal O-rings, are used in applications requiring higher pressure and temperature resistance. These sealing rings are often made from stainless steel or other alloys, providing exceptional strength and durability. Metal rings are commonly used in valves, flanges, and other high-pressure systems.
2.4. Lip Seals
Lip seals, also known as oil seals or radial shaft seals, are used to prevent the escape of fluids and contaminants in rotating equipment, such as pumps and motors. These sealing rings have a flexible lip that creates a barrier between the shaft and housing, ensuring proper lubrication and preventing leaks.
3. Applications of Sealing Rings in the Chemical Industry
3.1. Pumps and Compressors
Sealing rings are essential in pumps and compressors to prevent leakage and maintain efficiency. Whether it's centrifugal pumps, diaphragm pumps, or reciprocating compressors, properly selected and installed sealing rings ensure optimal performance, reduce downtime, and prevent costly fluid leaks.
3.2. Valves and Fittings
Valves and fittings in the chemical industry require reliable sealing to control fluid flow and prevent leakage. Sealing rings play a critical role in ensuring tight seals in ball valves, gate valves, butterfly valves, and pipe fittings, allowing for precise control and safe operation of the equipment.
3.3. Reactors and Distillation Columns
Reactors and distillation columns, where chemical reactions and separations occur, must have robust sealing systems to prevent hazardous leaks. Sealing rings in these applications withstand extreme temperatures, pressure, and aggressive chemicals, ensuring the integrity of the equipment and the safety of the operators.
3.4. Tanks and Pipelines
Storage tanks and pipelines in the chemical industry rely on sealing rings to maintain the containment of hazardous substances. By preventing leaks and protecting against corrosion, sealing rings contribute to the safe storage and transportation of chemicals, minimizing the risk of accidents and environmental damage.
4. The Benefits of Using Sealing Rings in the Chemical Industry
4.1. Ensuring Safety and Preventing Leakage
The primary function of sealing rings in the chemical industry is to prevent the escape of hazardous substances. By creating a reliable seal, these rings minimize the risk of leaks, protecting both personnel and the environment from potential harm.
4.2. Enhancing Equipment Performance and Efficiency
Properly selected and installed sealing rings optimize the performance of equipment in the chemical industry. By ensuring tight seals, they prevent energy losses, improve efficiency, and reduce the need for frequent maintenance or repairs.
4.3. Minimizing Downtime and Maintenance Costs
Sealing rings that effectively prevent leaks help minimize downtime and maintenance costs in the chemical industry. By reducing the risk of unexpected equipment failures and leaks, businesses can maintain smooth operations and avoid costly production interruptions.
4.4. Complying with Industry Regulations and Standards
The use of appropriate sealing rings is essential for complying with industry regulations and standards in the chemical sector. These regulations often require specific sealing solutions to ensure the safe handling, storage, and transportation of chemicals, and non-compliance can result in severe penalties.
5. Frequently Asked Questions (FAQs) about Sealing Rings in the Chemical Industry
5.1. What are the main factors to consider when selecting sealing rings for chemical applications?
When selecting sealing rings for chemical applications, factors such as chemical compatibility, temperature resistance, pressure ratings, and material durability should be considered. It is crucial to choose sealing rings that can withstand the specific conditions and chemicals they will be exposed to.
5.2. How often should sealing rings be inspected and replaced?
The frequency of inspection and replacement of sealing rings depends on several factors, including the operating conditions, chemical compatibility, and manufacturer's recommendations. Regular inspections should be conducted to identify signs of wear, damage, or degradation and replace sealing rings accordingly.
5.3. Can sealing rings withstand extreme temperatures and corrosive chemicals?
Yes, sealing rings can be designed to withstand extreme temperatures and resist corrosive chemicals. Different materials, such as specialized elastomers, metals, or composite materials, are available to meet the specific requirements of various chemical applications.
5.4. Are there any specific installation or maintenance requirements for sealing rings?
Proper installation and maintenance are crucial for ensuring the effectiveness and longevity of sealing rings. Following manufacturer guidelines, using appropriate lubrication, and conducting regular inspections are essential practices to maximize the performance of sealing rings.
5.5. Can sealing rings be customized for unique chemical industry needs?
Yes, sealing rings can be customized to meet unique needs in the chemical industry. By collaborating with experienced sealing ring manufacturers, businesses can have sealing rings tailored to their specific applications, ensuring optimal performance and safety.
6. Conclusion
In conclusion, sealing rings play a vital role in the chemical industry by ensuring safety, efficiency, and compliance with industry regulations. With various types available, including O-rings, gaskets, metal rings, and lip seals, businesses can choose appropriate sealing solutions for different applications. By preventing leaks, enhancing equipment performance, and minimizing maintenance costs, sealing rings contribute to the success and sustainability of chemical operations.
1. Introduction: Understanding the Significance of Sealing Rings in the Chemical Industry
2. Types of Sealing Rings Used in the Chemical Industry
2.1. O-Rings
2.2. Gaskets
2.3. Metal Rings
2.4. Lip Seals
3. Applications of Sealing Rings in the Chemical Industry
3.1. Pumps and Compressors
3.2. Valves and Fittings
3.3. Reactors and Distillation Columns
3.4. Tanks and Pipelines
4. The Benefits of Using Sealing Rings in the Chemical Industry
4.1. Ensuring Safety and Preventing Leakage
4.2. Enhancing Equipment Performance and Efficiency
4.3. Minimizing Downtime and Maintenance Costs
4.4. Complying with Industry Regulations and Standards
5. Frequently Asked Questions (FAQs) about Sealing Rings in the Chemical Industry
5.1. What are the main factors to consider when selecting sealing rings for chemical applications?
5.2. How often should sealing rings be inspected and replaced?
5.3. Can sealing rings withstand extreme temperatures and corrosive chemicals?
5.4. Are there any specific installation or maintenance requirements for sealing rings?
5.5. Can sealing rings be customized for unique chemical industry needs?
6. Conclusion
1. Introduction: Understanding the Significance of Sealing Rings in the Chemical Industry
In the chemical industry, where hazardous substances, high pressures, and extreme temperatures are common, sealing rings play a crucial role in maintaining safety, ensuring efficiency, and preventing costly leaks. These vital components provide a reliable barrier between different parts of equipment, preventing the escape of fluids or gases and keeping contaminants out.
2. Types of Sealing Rings Used in the Chemical Industry
2.1. O-Rings
O-rings are one of the most commonly used sealing rings in the chemical industry. They are circular rubber or elastomer rings designed to fit into a groove and create a seal between two mating surfaces. O-rings offer excellent resistance to chemicals, high pressures, and temperature variations, making them suitable for various applications.
2.2. Gaskets
Gaskets are flat sealing rings typically made from materials such as rubber, metal, or composite. They are used to create a seal between two or more mating surfaces, preventing leakage. Gaskets are available in different shapes and sizes and are chosen based on the specific requirements of the equipment and chemicals involved.
2.3. Metal Rings
Metal rings, such as spiral wound gaskets or metal O-rings, are used in applications requiring higher pressure and temperature resistance. These sealing rings are often made from stainless steel or other alloys, providing exceptional strength and durability. Metal rings are commonly used in valves, flanges, and other high-pressure systems.
2.4. Lip Seals
Lip seals, also known as oil seals or radial shaft seals, are used to prevent the escape of fluids and contaminants in rotating equipment, such as pumps and motors. These sealing rings have a flexible lip that creates a barrier between the shaft and housing, ensuring proper lubrication and preventing leaks.
3. Applications of Sealing Rings in the Chemical Industry
3.1. Pumps and Compressors
Sealing rings are essential in pumps and compressors to prevent leakage and maintain efficiency. Whether it's centrifugal pumps, diaphragm pumps, or reciprocating compressors, properly selected and installed sealing rings ensure optimal performance, reduce downtime, and prevent costly fluid leaks.
3.2. Valves and Fittings
Valves and fittings in the chemical industry require reliable sealing to control fluid flow and prevent leakage. Sealing rings play a critical role in ensuring tight seals in ball valves, gate valves, butterfly valves, and pipe fittings, allowing for precise control and safe operation of the equipment.
3.3. Reactors and Distillation Columns
Reactors and distillation columns, where chemical reactions and separations occur, must have robust sealing systems to prevent hazardous leaks. Sealing rings in these applications withstand extreme temperatures, pressure, and aggressive chemicals, ensuring the integrity of the equipment and the safety of the operators.
3.4. Tanks and Pipelines
Storage tanks and pipelines in the chemical industry rely on sealing rings to maintain the containment of hazardous substances. By preventing leaks and protecting against corrosion, sealing rings contribute to the safe storage and transportation of chemicals, minimizing the risk of accidents and environmental damage.
4. The Benefits of Using Sealing Rings in the Chemical Industry
4.1. Ensuring Safety and Preventing Leakage
The primary function of sealing rings in the chemical industry is to prevent the escape of hazardous substances. By creating a reliable seal, these rings minimize the risk of leaks, protecting both personnel and the environment from potential harm.
4.2. Enhancing Equipment Performance and Efficiency
Properly selected and installed sealing rings optimize the performance of equipment in the chemical industry. By ensuring tight seals, they prevent energy losses, improve efficiency, and reduce the need for frequent maintenance or repairs.
4.3. Minimizing Downtime and Maintenance Costs
Sealing rings that effectively prevent leaks help minimize downtime and maintenance costs in the chemical industry. By reducing the risk of unexpected equipment failures and leaks, businesses can maintain smooth operations and avoid costly production interruptions.
4.4. Complying with Industry Regulations and Standards
The use of appropriate sealing rings is essential for complying with industry regulations and standards in the chemical sector. These regulations often require specific sealing solutions to ensure the safe handling, storage, and transportation of chemicals, and non-compliance can result in severe penalties.
5. Frequently Asked Questions (FAQs) about Sealing Rings in the Chemical Industry
5.1. What are the main factors to consider when selecting sealing rings for chemical applications?
When selecting sealing rings for chemical applications, factors such as chemical compatibility, temperature resistance, pressure ratings, and material durability should be considered. It is crucial to choose sealing rings that can withstand the specific conditions and chemicals they will be exposed to.
5.2. How often should sealing rings be inspected and replaced?
The frequency of inspection and replacement of sealing rings depends on several factors, including the operating conditions, chemical compatibility, and manufacturer's recommendations. Regular inspections should be conducted to identify signs of wear, damage, or degradation and replace sealing rings accordingly.
5.3. Can sealing rings withstand extreme temperatures and corrosive chemicals?
Yes, sealing rings can be designed to withstand extreme temperatures and resist corrosive chemicals. Different materials, such as specialized elastomers, metals, or composite materials, are available to meet the specific requirements of various chemical applications.
5.4. Are there any specific installation or maintenance requirements for sealing rings?
Proper installation and maintenance are crucial for ensuring the effectiveness and longevity of sealing rings. Following manufacturer guidelines, using appropriate lubrication, and conducting regular inspections are essential practices to maximize the performance of sealing rings.
5.5. Can sealing rings be customized for unique chemical industry needs?
Yes, sealing rings can be customized to meet unique needs in the chemical industry. By collaborating with experienced sealing ring manufacturers, businesses can have sealing rings tailored to their specific applications, ensuring optimal performance and safety.
6. Conclusion
In conclusion, sealing rings play a vital role in the chemical industry by ensuring safety, efficiency, and compliance with industry regulations. With various types available, including O-rings, gaskets, metal rings, and lip seals, businesses can choose appropriate sealing solutions for different applications. By preventing leaks, enhancing equipment performance, and minimizing maintenance costs, sealing rings contribute to the success and sustainability of chemical operations.
Related News