-
AboutHebei Linaier Rubber Products Co., Ltd. is located in Duqiao Industrial Zone, Jingxian City, Hebei Province, adjacent to Dezhou, Shandong. Founded in early 2001 with a registered capital of 35 million yuan, it is a scientific

-
ProductMain products: vertical and horizontal imported and domestic filter plates, diaphragm plates, diaphragms and accessories; pinch valve sleeves and pinch valves and various mining accessories.
-
NewsIn 2013, our company's high-pressure cylinder with phenolic cloth support and guide ring obtained the national key new product certificate, project number: 2013GRA20011; its products in coal cylinders and engineering hydrauli
-
ServiceWe will actively cooperate with more enthusiasm, strengthen internal management, expand the market externally, improve various performance indicators of existing products, and truly achieve our win-win situation!
-
RecruitmentOur company always adheres to the talent concept of "people-oriented", provides a growth platform for talents, and realizes the common growth and development of enterprises and talents.


language
English
العربية
বাংলাদেশ
Български
Hrvatski
Česky
Dansk
Nederland
 Esperanto
Slovenski
Filipino
Suomi
Français
Maori
 Shqiptare
Georgian
 Euskara
Deutsch
Ελλάδα
ישראל
इंडिया
Magyarország
Ísland
Indonesia
Irlanda
Italia
日本語
Sovensko
Հայաստան
한국
Kyrgyz
ປະເທດລາວ
 Zulu
Latvian
Lithuanian
Luxembourgish
 Latinus
Macedonian
Малайская
Maltese
Монгол улс
 Cymraeg
ဗမာ
 தமிழ்
नेपाल
Norge
ایران
Polska
Portugal
România
Российская
Србија
 Slovak
Србија
 Slovak
Bosanski
Slovenian
Беларус
España
Sverige
Точик
ประเทศไทย
Türk
Azərbaycan
Uzbek
 Afrikaans
Việt Nam
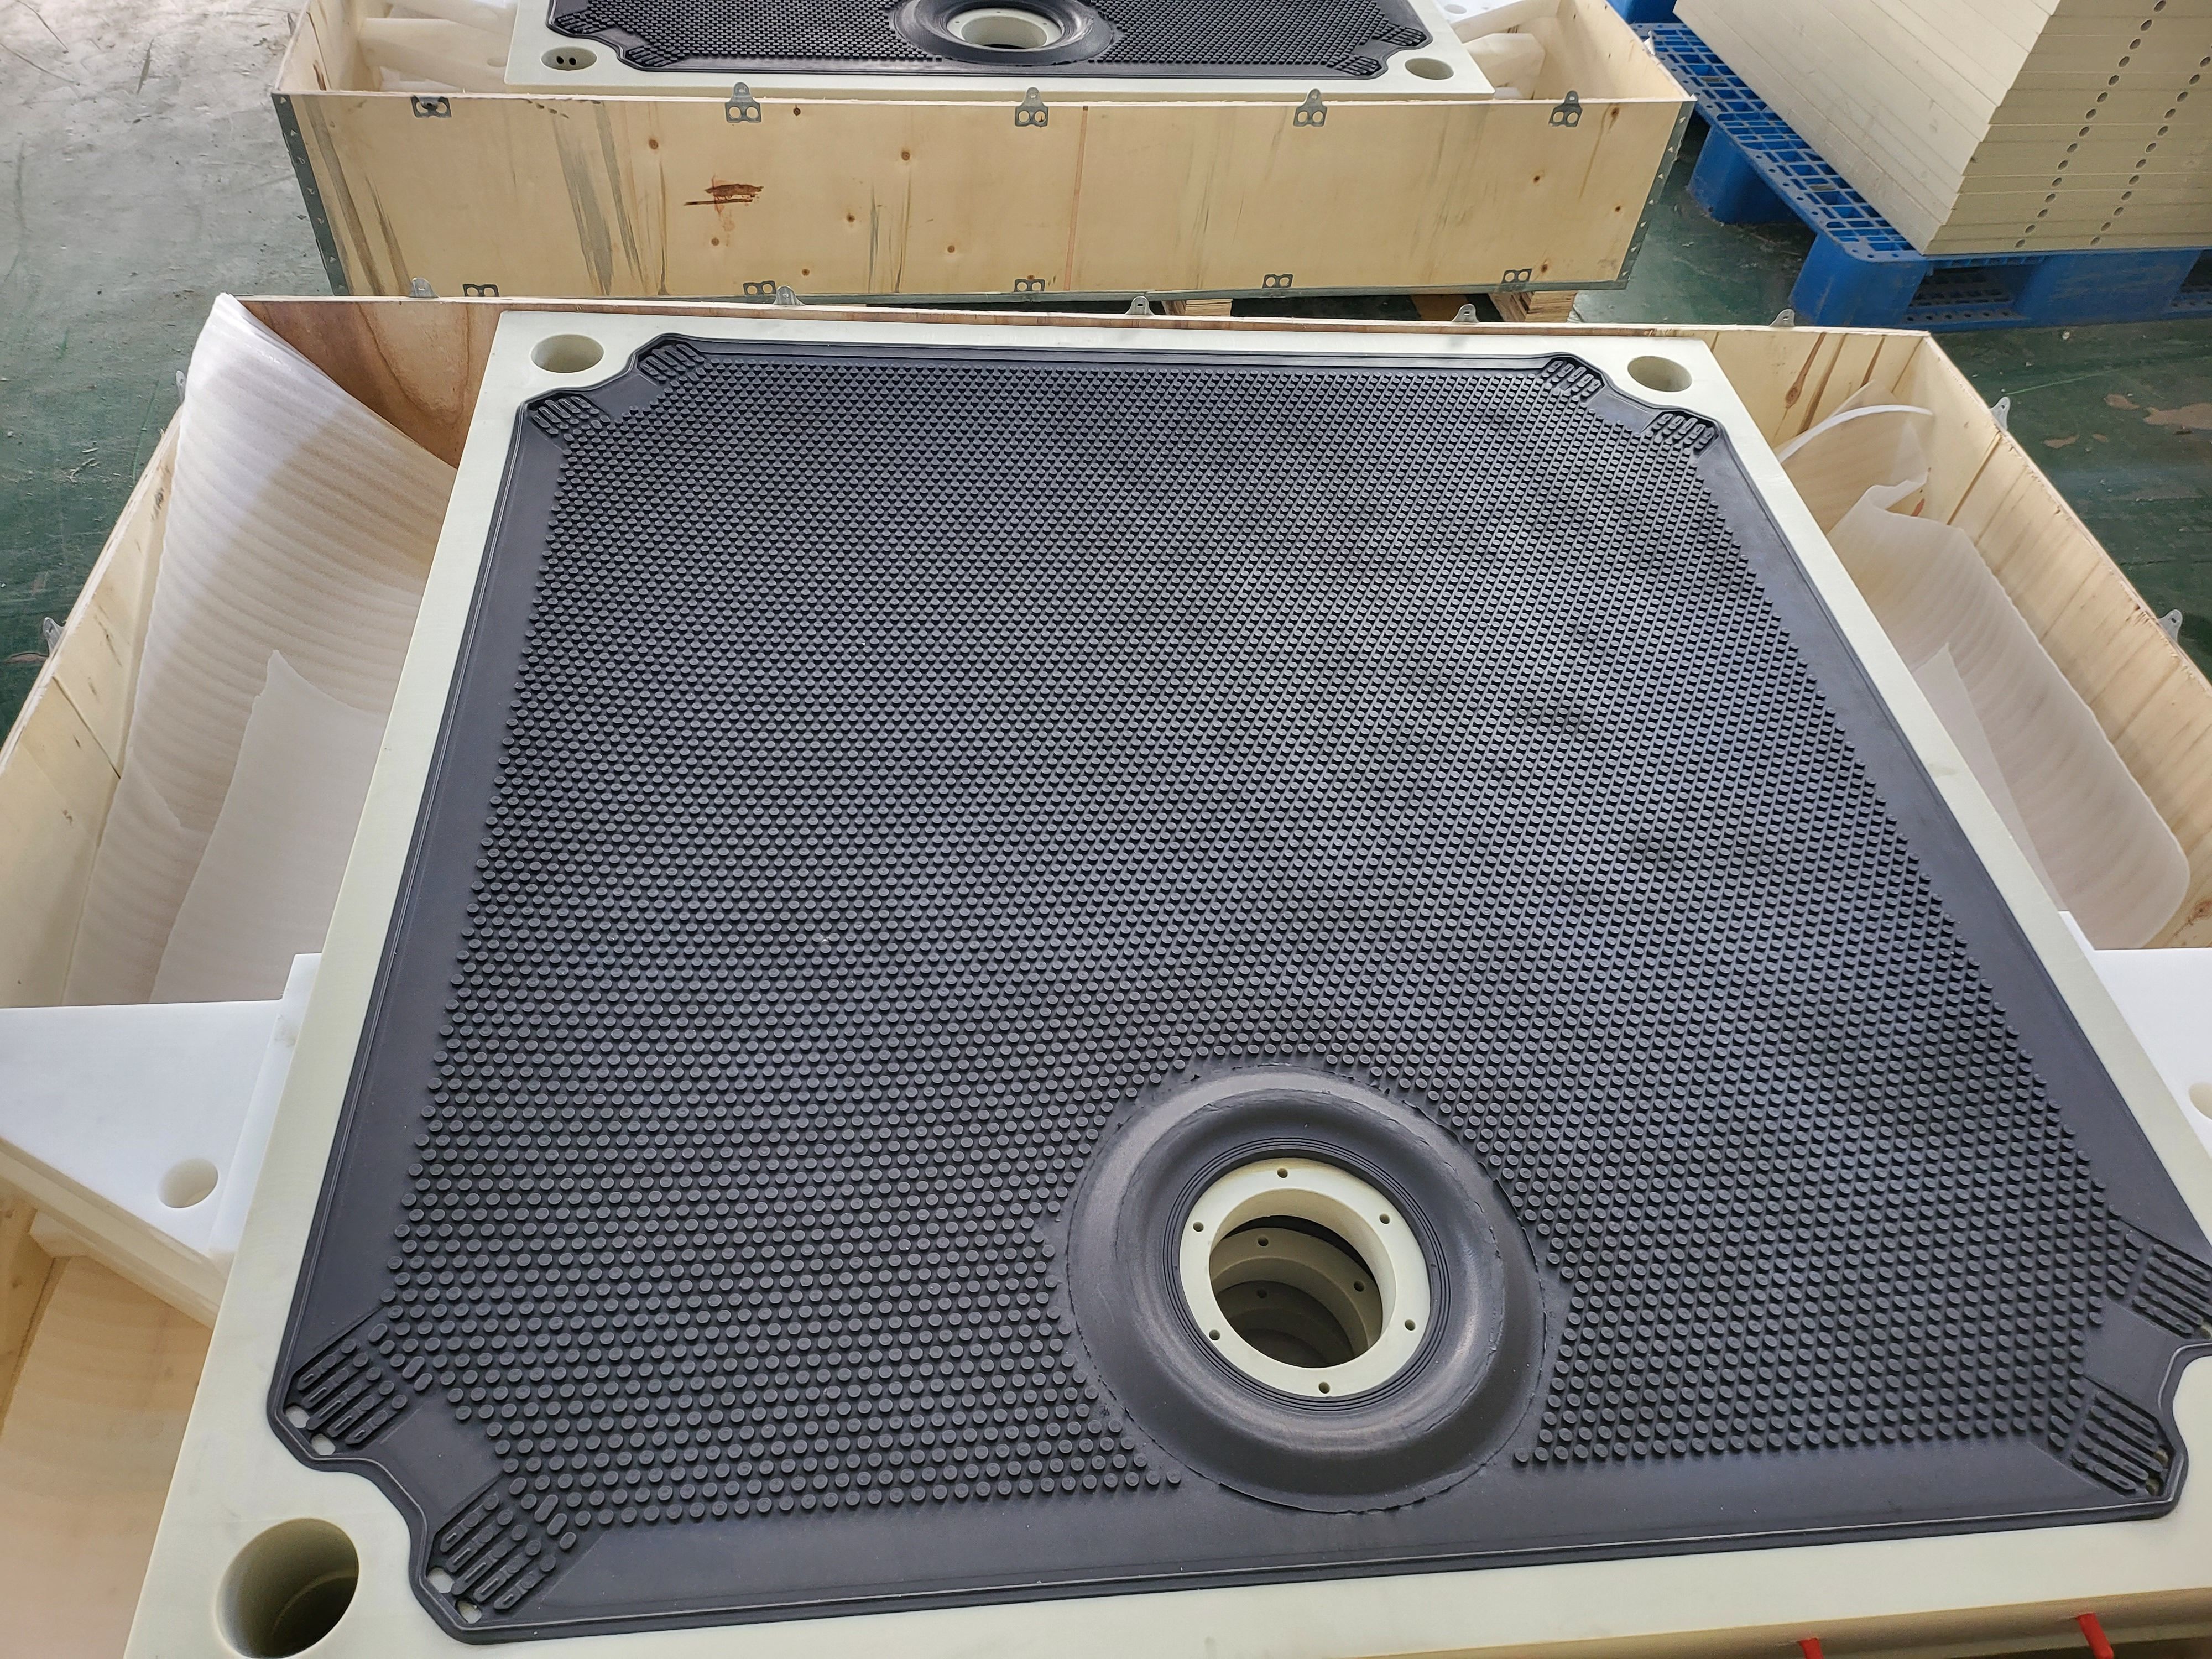
Introduction to 1.6㎡ Rubber Diaphragm in Chemical Industry
Release time:
2023-08-06
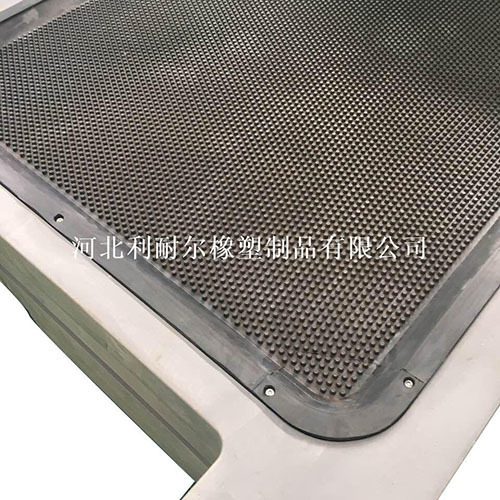
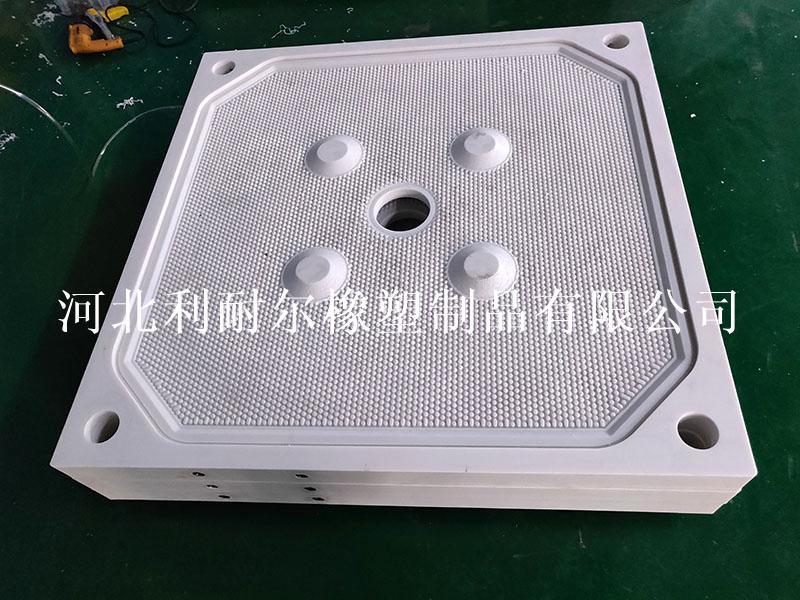
Title: Unveiling the Potential of 1.6㎡ Rubber Diaphragm in the Chemical Industry Introduction: Rubber diaphragms are vital components in the chemical industry, particularly in the realm of plastic and its derivatives. Among these, 1.6㎡ rubber diaphragms play a crucial role in ensuring seamless operations and facilitating precision control in numerous applications. Let's delve into the fascinating
Title: Unveiling the Potential of 1.6㎡ Rubber Diaphragm in the Chemical Industry
Introduction:
Rubber diaphragms are vital components in the chemical industry, particularly in the realm of plastic and its derivatives. Among these, 1.6㎡ rubber diaphragms play a crucial role in ensuring seamless operations and facilitating precision control in numerous applications. Let's delve into the fascinating world of 1.6㎡ rubber diaphragms and explore their significance in the chemical industry.
1. High Durability:
1.6㎡ rubber diaphragms are renowned for their exceptional durability, making them suitable for demanding and harsh operating conditions. Their robust construction enables them to withstand mechanical stress and fluctuations in temperature, ensuring consistent performance over an extended period.
2. Chemical Resistance:
One of the standout properties of 1.6㎡ rubber diaphragms is their exceptional resistance to various chemicals. This characteristic is particularly vital in the chemical industry, where exposure to aggressive substances is commonplace. These diaphragms effectively resist corrosion, deterioration, and degradation caused by contact with acids, alkalis, solvents, and other aggressive chemicals.
3. Flexibility and Elasticity:
The flexibility and elasticity of 1.6㎡ rubber diaphragms enable them to conform to the unique shape and requirements of different equipment and systems. They can be easily molded and customized to fit various dimensions, providing an effective sealing solution for valves, actuators, pumps, and other critical components. This versatility enhances operational efficiency and minimizes the risk of leakage, ensuring smooth and consistent performance.
4. Precise Control:
In the chemical industry, accurate control of fluid flow, pressure, and volume is of utmost importance. 1.6㎡ rubber diaphragms excel in this regard, offering precise and responsive control due to their inherent ability to expand and contract rapidly. This characteristic makes them ideal for applications such as metering, dosing, regulating, and proportional control systems.
5. Applications:
The applications of 1.6㎡ rubber diaphragms in the chemical industry are vast. They find extensive use in areas such as pneumatic and hydraulic control systems, dosing pumps, solenoid valves, vacuum pumps, pressure regulators, and many more. Their reliable performance and compatibility with aggressive chemicals make them indispensable in maintaining safety, efficiency, and productivity in various chemical processes.
In conclusion, 1.6㎡ rubber diaphragms are essential components in the chemical industry, playing a pivotal role in ensuring precise control, durability, and chemical resistance. Their versatile applications and functional properties make them indispensable in various industrial processes. Understanding the significance of these diaphragms can aid professionals in the chemical industry in choosing the right solution for their specific requirements, ultimately enhancing productivity and operational efficiency.
Related News